Printable Version of Topic
Click here to view this topic in its original format
914World.com _ 914World Garage _ Fred's 2374 -> 2258 Engine Build Thread
Posted by: friethmiller Jun 26 2026, 03:07 PM
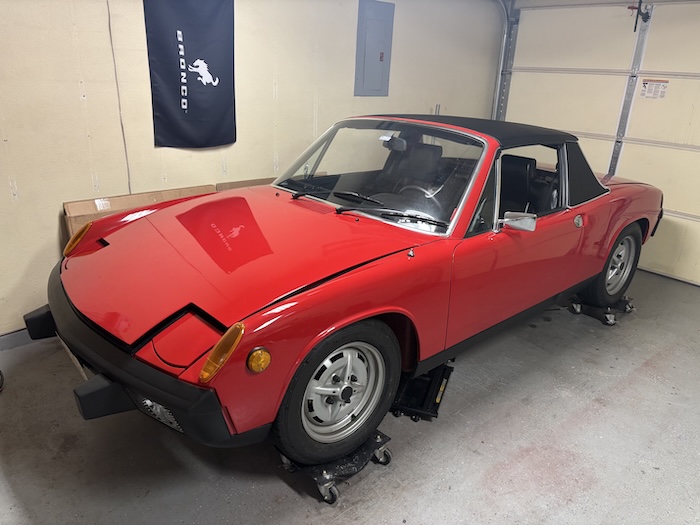
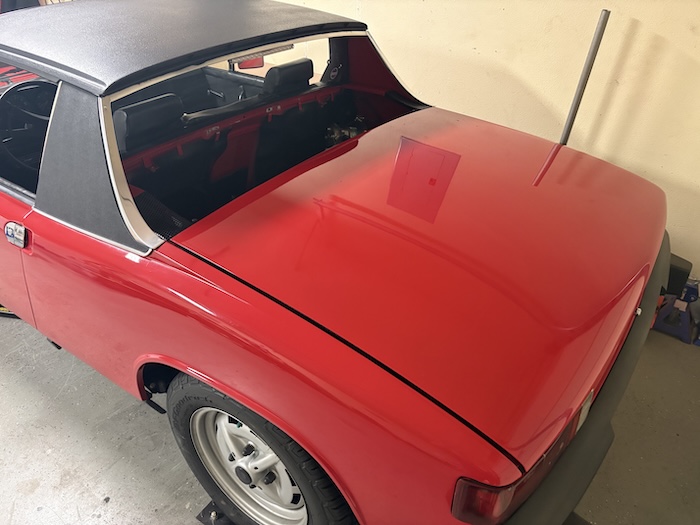
I can't believe it but after 1-1/2 years of waiting for my engine components to be machined, I am finally picking up the parts tomorrow  . I will post more after talking to the owner about the issues he found with my case. This is what was holding everything up. Luckily. I have source another case (from my shed) and will be using this one instead. Here's a few pics of the my "other '74" after uncovering it today and wiping off a bit of dust. She needs to ride again! Hoping for Okteenerfest. Stay tuned!
Posted by: Ron914 Jun 26 2026, 04:59 PM

I can't believe it but after 1-1/2 years of waiting for my engine components to be machined, I am finally picking up the parts tomorrow
. I will post more after talking to the owner about the issues he found with my case. This is what was holding everything up. Luckily. I have source another case (from my shed) and will be using this one instead. Here's a few pics of the my "other '74" after uncovering it today and wiping off a bit of dust. She needs to ride again! Hoping for Okteenerfest. Stay tuned! Car looks great . Did this one start out like the Bumblebee ?
Posted by: 930cabman Jun 26 2026, 05:35 PM
Been holding out eh
Posted by: friethmiller Jun 26 2026, 07:54 PM
Car looks great . Did this one start out like the Bumblebee ?
Yes, it was just as “awesome” as the LE. The hell hole was especially fun. Here are a few pics - just for you


Posted by: friethmiller Jun 26 2026, 07:58 PM
Turned out alright, I think. Learned a lot!
Posted by: Ninja Jun 26 2026, 08:47 PM
SHOW OFF!!
An engine thread needs ENGINE pictures!
We all know you can work the metal just fine...
Get with the greasy stuff!

Posted by: friethmiller Jun 26 2026, 09:05 PM
Hee, hee… yes, it’ll all start tomorrow, Rick.
Posted by: friethmiller Jun 27 2026, 05:16 PM
Initial Layout (6/27/2026):
After about 5 hours of driving to go get my engine parts, I got home just after lunchtime today. I started laying things out in an attempt to get things organized. I took a few pictures. As I mentioned earlier, my original EA case will not be used on this build. Instead, I will be using my back-up W-case that I had machined late last year. The problem with the EA case is that 2 of the mains are too tight. So this case probably needs align bore. I'll do this at a later date. Hell, I've got the LE case getting worked on at the moment. The machinist bill is high enough at the moment - thank you.
Here's a pic the W-case on the stand. This was align-bored .20, oil-galleys tapped, with the cylinder openings just cleaned-up (no need for decking). Work was done by EMW in 2025.
The dual-spring 1.8L heads were cleaned, inspected, and reassembled. These heads were previously reconditioned [back in 2020] and checked out fine. They are port & polished with 44/38 valves.

Going with a new 78mm crank. This is why my 2.3L will become a 2.2L.
Pistons are new 96mm forged JEs with ceramic coating on the sides and top. Rods checked out fine but were modified for better oiling. Note off-center oil grooves.

Cylinders are original German 93mm, 1.8L units that were sandblasted, painted with flat black paint, and then bored to 96mm
During this layout I ran across two different cams that I had purchased last year for this build. I think I'd like to go with the 163/86b for this one. We'll see. Would like input from others on this choice. More to come soon. Cheers! 


Posted by: seanpaulmc Jun 27 2026, 05:57 PM
I’m so excited and it’s not even my car. 
1. Who’s crank?
2. Is that oiling groove on both sides of the connecting rod?
Looking forward to watching this come together. 
Cheers,
Sean
Posted by: Jack Standz Jun 27 2026, 06:05 PM
Hi Fred,
Me thinks that's a great cam choice. It's pretty much what Raby developed and sold (maybe with a different LSA, not sure?).
Might want to run it a little advanced. We have two new ones (163/86b) in the boxes for upcoming projects, but was a little disappointed that we could only get them with 104 degrees lobe separation. But, understand that "custom" cams are months and months and months away. 
Webcams makes good cams, so hoping you (and we) are happy with them!
Posted by: Montreal914 Jun 27 2026, 06:19 PM
WOW, super cool!! Where to begin my comments...
First: hell hole? What hell hole? I am seeing more an abyss!
That car looks beatiful! Did you install the braces for the inner suspension ears? I am seeing the anchor point on the firewall.
Good looking engine parts! 
Do yo have the matching lifters for that WebCam camshaft?
EDIT: is there a reason why the notch in the connecting rod is offset instead of centered?
Very soon you will have too many restored 914s, what will you do? 
Posted by: friethmiller Jun 27 2026, 06:40 PM
I’m so excited and it’s not even my car.
1. Who’s crank?
2. Is that oiling groove on both sides of the connecting rod?
Looking forward to watching this come together.
Cheers,
Sean
1. I think this is a AA performance forged chromoly crank
2. Yes. The machinist has a lot of experience with VW engines. He said he prefers an offset 'U' groove on both sides of the rod. He mentioned better directed oil spray at the bottom of the piston. I assume the groove would need to be on the top but will verify with him before assembly.
Posted by: Puebloswatcop Jun 27 2026, 06:44 PM
I can't believe it but after 1-1/2 years of waiting for my engine components to be machined, I am finally picking up the parts tomorrow
. I will post more after talking to the owner about the issues he found with my case. This is what was holding everything up. Luckily. I have source another case (from my shed) and will be using this one instead. Here's a few pics of the my "other '74" after uncovering it today and wiping off a bit of dust. She needs to ride again! Hoping for Okteenerfest. Stay tuned! Fred, If she needs some TLC, I would be happy to come over and take her for daily trips so she doesn't get boared.......lol
Posted by: friethmiller Jun 27 2026, 06:45 PM
Did you install the braces for the inner suspension ears? I am seeing the anchor point on the firewall.
Do yo have the matching lifters for that WebCam camshaft?
Yes, I installed Tangerine Racing's "Rear Suspension Inner Pickup Heim Rod Brace Kit" on this car. Easy upgrade if you have the welder out.

Good Question on the lifters. I have a set of LN Engineering solid lifters. I know Web calls for their own lifters. The LNs are obviously high-quality. Do you think using them would be ok?
Posted by: Ninja Jun 27 2026, 06:55 PM
Ah, meat and potatoes...
Thank you!
So, 2258 with flat tops and the 1.8 heads.
Have you figured compression?
Parts look nice!
Posted by: friethmiller Jun 27 2026, 07:16 PM
Ah, meat and potatoes...
Thank you!
So, 2258 with flat tops and the 1.8 heads.
Have you figured compression?
Parts look nice!
Yes. I'm targeting 9.1 - 9.2, depending on deck height. The chambers are 60cc with a 0.9cc valve pocket in the pistons.
Posted by: friethmiller Jun 27 2026, 07:19 PM
Fred, If she needs some TLC, I would be happy to come over and take her for daily trips so she doesn't get boared.......lol
You're such a good friend, Kevin. I appreciate your willingness to help out.
Posted by: 914werke Jun 27 2026, 07:43 PM
Curious , why offset as the published description of this mod was centered ?

Posted by: Montreal914 Jun 27 2026, 07:49 PM
Did you install the braces for the inner suspension ears? I am seeing the anchor point on the firewall.
Do yo have the matching lifters for that WebCam camshaft?
Yes, I installed Tangerine Racing's "Rear Suspension Inner Pickup Heim Rod Brace Kit" on this car. Easy upgrade if have the welder out.
Good Question on the lifters. I have a set of LN Engineering solid lifters. I know Web calls for their own lifters. The LNs are obviously high-quality. Do you think using them would be ok?
For a good time (not sure today), WebCam was supplying cams to Raby. One of his popular version for that size engine was the 163/86b but with a twist. I assume yours is also on a 1.063" base circle to clear the connecting rods?
With larger induction you will get more power out of the 86B/86C but all of this is with heads that flow. Your 1.8 heads will have limitations.
All of this is information I have read over the years and wrote down in my notebook.
 You should check everything. I would definitely make a call to WebCam.
I visited the ladies a few years back when I was planining on building a 2258 for my project and they were very helpful and happy to answer questions. I too was going to use the 163/86b for a good all around cam (civilised
).All this to say that your LN lifters may be WebCam ones.
Posted by: friethmiller Jun 27 2026, 08:35 PM
Curious , why offset as the published description of this mod was centered ?
Rich, I think it’s a matter of cooling the piston vs the wrist pin. Not 100% sure. I’ll get more details on Monday.
Posted by: friethmiller Jun 27 2026, 08:59 PM
All this to say that your LN lifters may be WebCam ones.
Right! I will find out. Here are the cards from both cams. 104 lc on both.


FYI, my intake/exhaust valves are 44/38 and my exhaust is a full 1 5/8” tangerine header + muffler.
Posted by: friethmiller Jun 28 2026, 04:47 PM
Trying to verify dimensions here. What is the standard case bore for the type 4 engine? AI says 2.559”. That seems too small. I’m measuring roughly 2.768 for the rear main on a case with a .02 line bore. Why am I off a decimal place? 
Posted by: 930cabman Jun 28 2026, 05:48 PM
Trying to verify dimensions here. What is the standard case bore for the type 4 engine? AI says 2.559”. That seems too small. I’m measuring roughly 2.768 for the rear main on a case with a .02 line bore. Why am I off a decimal place?
I had my local machinist make up a "case gage", it's a couple thou over to allow for some clearance. I can check tomorrow and report back
Posted by: cgnj Jun 28 2026, 06:06 PM
@http://www.914world.com/bbs2/index.php?showuser=22863 AI is not your friend. That is for a type 1 motor.
Type4 Saddle bore is 70mm or 2.756. 2.768 is correct
Posted by: friethmiller Jun 28 2026, 07:15 PM
@http://www.914world.com/bbs2/index.php?showuser=22863 AI is not your friend. That is for a type 1 motor.
Type4 Saddle bore is 70mm or 2.756. 2.768 is correct
Excellent! Thank you.

Posted by: friethmiller Jun 29 2026, 06:08 PM
Ok, I've confirmed two things.
- My EA block is too tight on #1, #2, and #3 saddles, as identified by my machinist.
- [Thankfully] My W-block checks out at .020 line bore
Photos of my work to measure each saddle in multiple directions. Will proceed with verifying my brand new crank next before preparing for assembly. So far so good.


Thanks again to @http://www.914world.com/bbs2/index.php?showuser=403 for the specs!
Posted by: Montreal914 Jun 29 2026, 07:02 PM
Good news! 
Nice metrology tools btw.
Did you get a chance to measure the bearings?
Posted by: Ninja Jun 29 2026, 07:11 PM
Are bearings MORE available if you need .020 over on the OD?
I thought main bearings were a bit on the scarce side right now.
Nice work Fred!
Posted by: zig-n-zag Jun 29 2026, 09:34 PM
Yes, nice tools you have there.
With the main bearing tunnel being tight, ask your machinist if doing a line
hone can be achieved to re-new the saddles back to standard bearing size?
Posted by: Jack Standz Jun 29 2026, 10:25 PM
Are bearings MORE available if you need .020 over on the OD?
I thought main bearings were a bit on the scarce side right now.
Nice work Fred!
AApistons.com shows some .020 case/main bearings available, but not for std crankshaft size. So, depends on what his crankshaft measures at.
Maybe someone else will have the right size. We had a very hard time finding main bearings earlier this year for one motor. The other motor we fortunately already had the proper bearings.
Posted by: friethmiller Jun 30 2026, 07:04 AM
With the main bearing tunnel being tight, ask your machinist if doing a line
hone can be achieved to re-new the saddles back to standard bearing size?
Yes, after I build this motor with my W block, I will likely send the EA block out to be checked and line bored correctly to .020. After waiting for so long for machine work on this build I want, at a minimum, a short block sitting in my garage ready to go. The EA motor will be my back-up
Posted by: friethmiller Jun 30 2026, 07:17 AM
Good news!
Did you get a chance to measure the bearings?
Are bearings MORE available if you need .020 over on the OD?
AApistons.com shows some .020 case/main bearings available, but not for std crankshaft size. So, depends on what his crankshaft measures at.
I just ordered another set of .020/std bearings last night from LN, just in case. The crank is brand new so it should measure as STD. @http://www.914world.com/bbs2/index.php?showuser=12023 , I started looking at the two sets of bearing I do have on-hand. One looks like std/std, which is unobtainium at them moment. The other set is .020/std, however, the split bearing in the box doesn't match the others. These bearings sat in a box at the machine shop and I don't trust what might have happened to them. The Mahle line-bore (.020) bearings are sold out on AA. The do have some Silverline but not at .020/std as @http://www.914world.com/bbs2/index.php?showuser=23644 mentioned. So, @http://www.914world.com/bbs2/index.php?showuser=29004 - I think you can still find other non std/std but even those are a bit scarce at the moment.
Posted by: Ninja Jun 30 2026, 08:57 AM
I have another question...
How do the main bearing journals get TIGHT????
All the damage I've ever seen INCREASES the bores.
In a normal engine the parting surfaces (both block and cap) get a couple of thousands machined off to reduce the diameter and then a line bore is done back to standard size.
Exception is a "cracked" cap (GM LS series rods) where bore is increased and oversized OD bearings are used.
Never seen/heard about undersized main journals until your thread...
Posted by: friethmiller Jun 30 2026, 09:06 AM
I have another question...
How do the main bearing journals get TIGHT????
All the damage I've ever seen INCREASES the bores.
In a normal engine the parting surfaces (both block and cap) get a couple of thousands machined off to reduce the diameter and then a line bore is done back to standard size.
Exception is a "cracked" cap (GM LS series rods) where bore is increased and oversized OD bearings are used.
Never seen/heard about undersized main journals until your thread...
Improper prior machine work, is my guess. The place that did it is no longer in business.
Posted by: Nogoodwithusernames Jun 30 2026, 09:21 AM
Fred,
If mains are tight, I would see if the shop can machine them just to STD. No need to go overbore, especially for a "down the road" type project.
Posted by: friethmiller Jun 30 2026, 02:25 PM
Ok, three things to report back on. I talked with the machinist and called Web Cams today.
1) The Machinist said he offsets the oil grooves to better cool the bottom of the piston and still splash the wrist pin.
2) He also measured that the saddles #1-#3 on my EA case were all tight. He said he measured between .002 and .0027. This is in line with what I'm measuring. So that gives us a bore between 2.7733" - 2.774". Thats shy of the expected 2.776" for a .020 line bore. Note: #4 (smaller) saddle is spot on. This is a [previous] machining error in my book. Like I said earlier, I'll send this case to get bored to the correct dimensions.
3) The lady at Web Cam said that LN Engineering buys their cams for their builds but they don't buy Web Cam's lifters. She said that both lifters likely derived from the same scat origins and that I'm safe to proceed with using the LN lifters.
Posted by: friethmiller Jul 1 2026, 11:41 AM
Please help play.... read the micrometer! This is a 2-3" micrometer. I get 2.776. I hope I'm wrong.
Posted by: cgnj Jul 1 2026, 12:35 PM
I'm watching now because you lost me.
Posted by: Ninja Jul 1 2026, 01:21 PM
Please help play.... read the micrometer! This is a 2-3" micrometer. I get 2.776. I hope I'm wrong.
Yep!
I'm seeing 2.776 too!
I'm ALSO seeing a cheap mic.
Do you have a 2" and 3" standards?
I'd want those to zero that mic.
One of my favorite mics is a Starrett 1.5-2.5 mic that can be zeroed at the center point with a 2" standard.
Cheap mics can work KICK-ASS but a known accurate standard is a must...
The method you were using the bore gauge (setting zero to your required measurement) is the ONLY way to go in my book.
Hats off to you Sir!
Many so called "machinist" don't do it that way.
Using one tool to determine your clearance is far more accurate than using two
Posted by: friethmiller Jul 1 2026, 01:37 PM
Do you have a 2" and 3" standards?
I'd want those to zero that mic.
I'm thinking this must be my problem. I swear this W case spec'd out the other day but when I rechecked it yesterday it was .002 - .003 too large. I have a 2" inch standard. let me verify/reset the mic.
Posted by: Shivers Jul 1 2026, 01:44 PM
Nice parts Fred
Posted by: zig-n-zag Jul 2 2026, 02:53 AM
A tip I got long ago was to always store engine cases bolted together to
prevent warping. Check the camshaft saddle under the #2 bearing to see
if it had collapsed or rocks using a straight edge. Run the straight edge
horizontally over all 3 cam saddles, on both sides of the saddles, and
vertically over the #2 main bearing saddle, and out to the case perimeters.
A problem there might mean a cam tunnel line bore. And there’s 1 more
check to do. Bolt the case together with the 6 big nuts and torque it to
25lbs. Back light the center main at the parting face. If you see any light
between the parting faces, that means you’ll have low oil pressure,
because oil will be leaking out from the back side of the bearing.
Posted by: friethmiller Jul 2 2026, 06:03 AM
A tip I got long ago was to always store engine cases bolted together to
prevent warping. Check the camshaft saddle under the #2 bearing to see
if it had collapsed or rocks using a straight edge. Run the straight edge
horizontally over all 3 cam saddles, on both sides of the saddles, and
vertically over the #2 main bearing saddle, and out to the case perimeters.
A problem there might mean a cam tunnel line bore. And there’s 1 more
check to do. Bolt the case together with the 6 big nuts and torque it to
25lbs. Back light the center main at the parting face. If you see any light
between the parting faces, that means you’ll have low oil pressure,
because oil will be leaking out from the back side of the bearing.
Will do! It's together with the case bolts torqued at the moment. I'll start with the backlighting one first. Thanks!
UPDATE: It all looks fine. Everything checks flat and no light can be seen between any of the saddle parting lines.
Posted by: friethmiller Jul 2 2026, 08:29 AM
To summarize my current issue, I'm measuring my W case with a 0.020 bore at 0.022 - 0.023. I have a new 2-3" micrometer coming in tomorrow. If the results are the same, I'm sending out the EA block to get fixed or sourcing another case. 
So, until I'm satisfied with the case measurements, I'm NOT proceeding. Doing so is a fool's errand.
Posted by: Nogoodwithusernames Jul 2 2026, 02:20 PM
To summarize my current issue, I'm measuring my W case with a 0.020 bore at 0.022 - 0.023. I have a new 2-3" micrometer coming in tomorrow. If the results are the same, I'm sending out the EA block to get fixed or sourcing another case.
So, until I'm satisfied with the case measurements, I'm NOT proceeding. Doing so is a fool's errand.
Have you checked it with bearings installed? With the variation in new bearings maybe you got lucky and have some bearings that are on the large size and will work with the case. I've heard of guys ordering multiple sets of bearings to get a fit they like.
Posted by: friethmiller Jul 2 2026, 03:43 PM
Have you checked it with bearings installed? With the variation in new bearings maybe you got lucky and have some bearings that are on the large size and will work with the case. I've heard of guys ordering multiple sets of bearings to get a fit they like.
Thanks @http://www.914world.com/bbs2/index.php?showuser=20051
Interesting... my second set of bearings just showed up today.
Posted by: friethmiller Jul 2 2026, 04:02 PM
Wanted to verify the oil clearance on the mains. AI says:
0.03 mm to 0.08 mm (0.001" to 0.003") for journals #1, #2, and #3
0.05 mm to 0.10 mm (0.0019" to 0.004") on journal #4
Does this sound correct or is this AI screwing up and giving me Type 1 specs? I think .002 is desired, if I'm remembering correctly. TIA.
Posted by: 930cabman Jul 2 2026, 04:17 PM
Wanted to verify the oil clearance on the mains. AI says:
0.03 mm to 0.08 mm (0.001" to 0.003") for journals #1, #2, and #3
0.05 mm to 0.10 mm (0.0019" to 0.004") on journal #4
Does this sound correct or is this AI screwing up and giving me Type 1 specs? I think .002 is desired, if I'm remembering correctly. TIA.
Those clearances look good to me, have you installed the crank/bearings with a bit of oil, torqued the case bolts and see how she spins?
Posted by: friethmiller Jul 2 2026, 05:32 PM
Not yet. I’m asking if these are the recommended clearances. I’m about to start measuring crank to bearing clearances. I will be mic’ing the main journal, zeroing the dimension to my bore gauge, and then measuring the clearance with the bearings mounted/torqued in the case.
Posted by: friethmiller Jul 5 2026, 07:45 PM
Update:
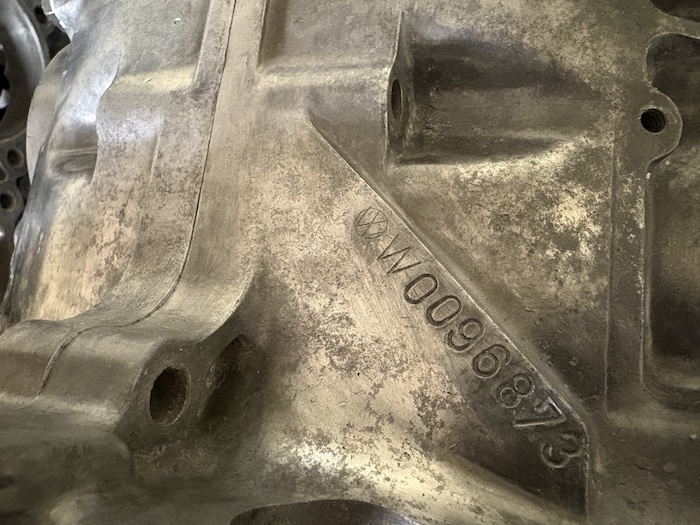
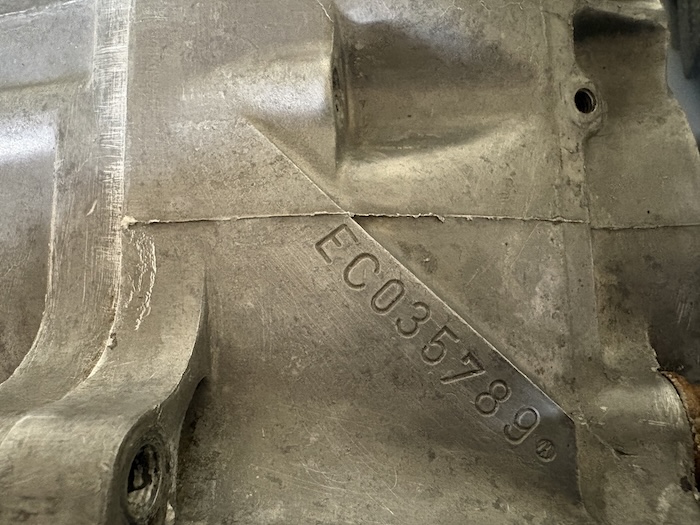
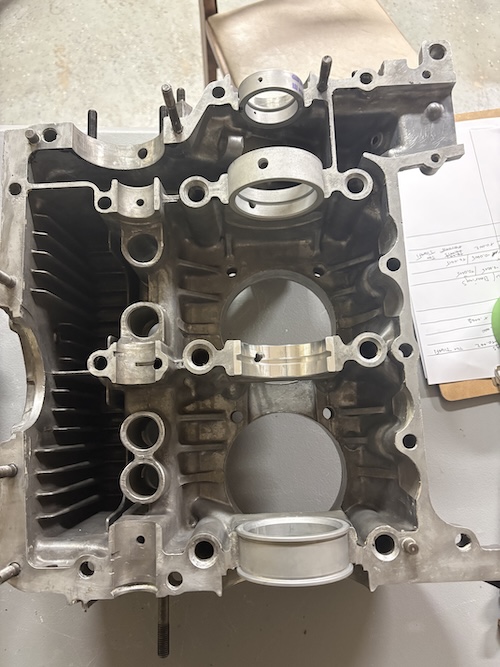
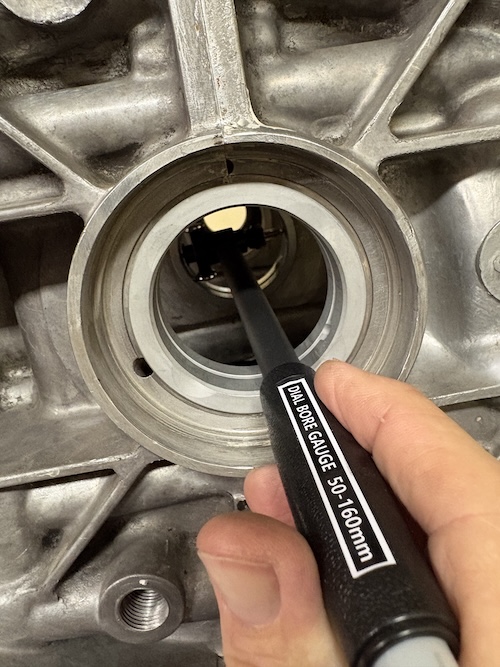
I spent a lot of time this weekend in the garage attempting to get good measurements on both my EC and W cases. While I measured the EC block's saddles a little tight, the W case measured a little loose from the .20 bore specs. However, once the .50/STD bearings were installed in the cases things changed a bit.
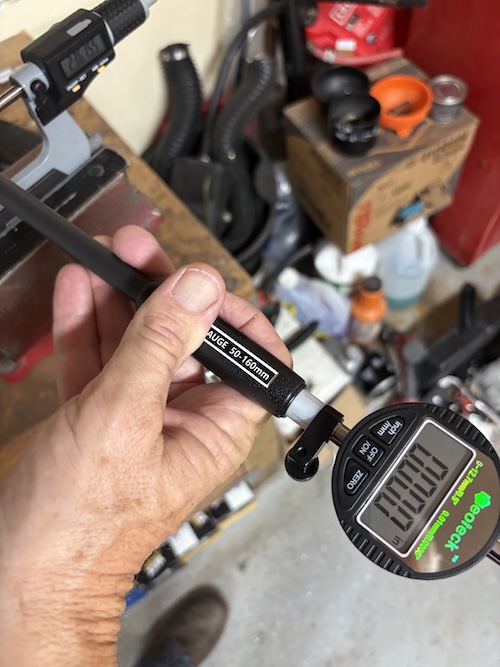
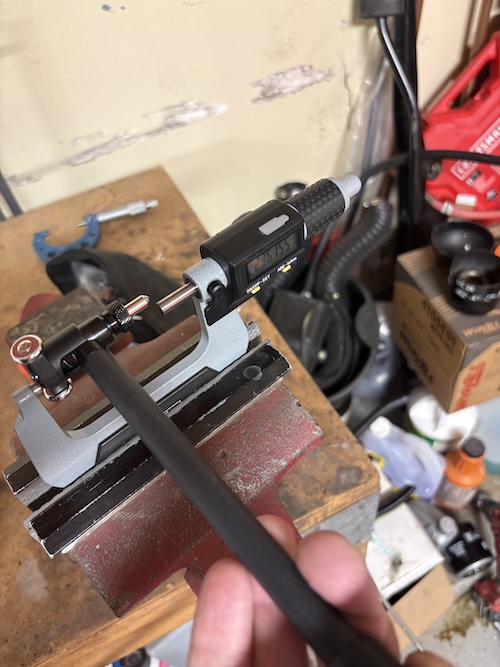
The saddle measurements where taken in relationship to a book value of 2.776 +/- .0004. I basically adjusted my 2-3" micrometer (zeroed with a 2" standard) to 2.776" and locked it in a vise. Next, I took my bore gauge and zeroed in the micrometer. From here, I measured roughly in the 9-3 o'clock and the 12-6 o'clock positions.
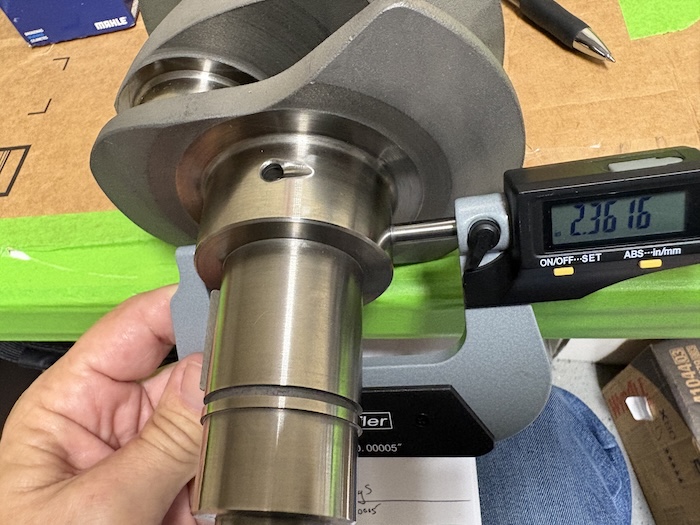
To determine the bearing clearance, I first measured the crank main journals with the digital 2-3" micrometer. From my measurements, all 3 main bearings were 2.3616". Locking in this value, I then clamped the micrometer in the vice and zeroed the bore gauge to this value. From here I measured several times in each of the clock positions on either side of the oil groove for each bearing. I did this multiple times throughout Saturday and Sunday to come up with a set of clearances for each of the first 3 mains on both blocks. These numbers represent the "tightest obtainable value" in and around the measurement areas using the bore gauge.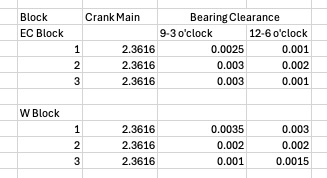
Not that these are set in stone. I want to continue working the instruments till I'm satisfied with all the numbers I'm getting. Repeatability is the word, I guess.
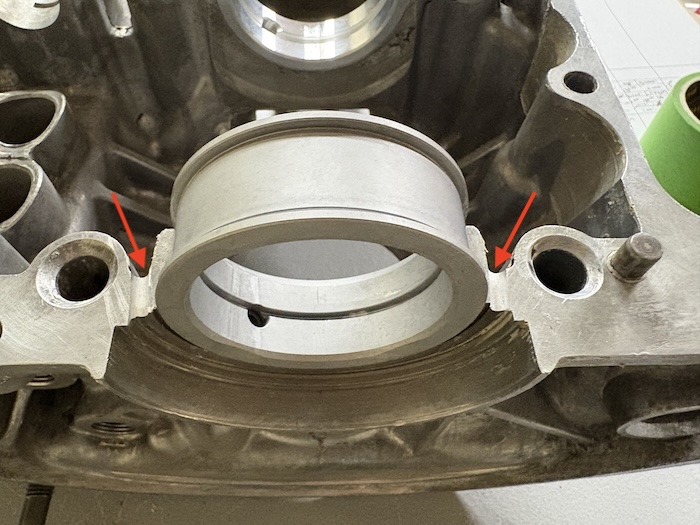
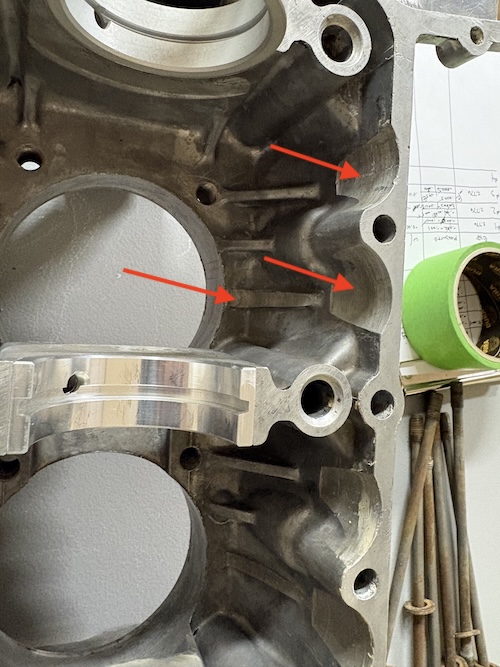
Including other photos I took while measuring the cases. Note the arrows showing the oil relief in the rear main of the EA Case as well as the "relief" areas that were required to handle the previously installed 82mm crank. We will be switching down to a more manageable 78mm unit with this build. 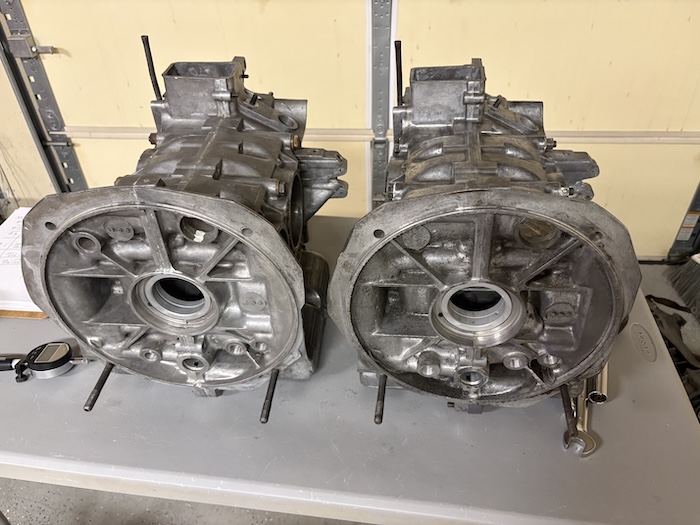
Posted by: friethmiller Jul 6 2026, 07:56 AM
W Case Measurements:
Went out to the garage this morning, pulled the bearings, re-torqued the case, and took the following saddle measurements of the W case. FYI, this case was line-bored back in January of 2025 by EMW. Note: Anything in red is out of range, yellow is borderline, and green is within tolerance. Positive numbers are larger than mid-range spec. Negative are smaller than the mid-range spec.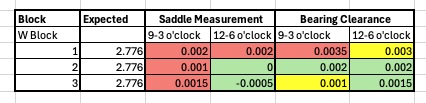
So, if my measurements are accurate, I'm unwilling to use this block as-is. I'll do the same work-up on my EA case at lunch. Let me know what y'all think. TIA.
Posted by: friethmiller Jul 6 2026, 03:20 PM
EA Case Measurements:
Ok, I might be alright. Here are the measurements for the EC case. The only adjustment I made was remeasuring my crank mains at 2.3617 instead of 2.3616. I felt I was a little "tight" on the journal when I took the original measurements.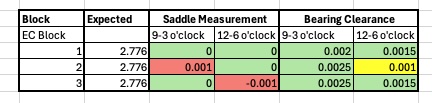
AI says having a slightly tighter measurement at the 12 o'clock position (along the parting line) is fine.
Posted by: friethmiller Jul 7 2026, 06:26 AM
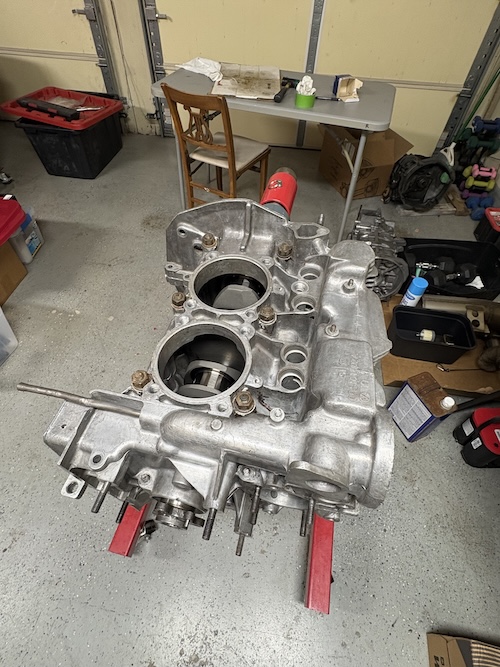
Initial Mockup
Used a light coating of assembly lub on the bearing surfaces and installed the crankshaft into the EC case. I checked for good rotation throughout the process. Installed the other case half, checked rotation, and then torqued the case in sequence. Final test was just the same. The crank moves freely 360 degrees by hand - no issues.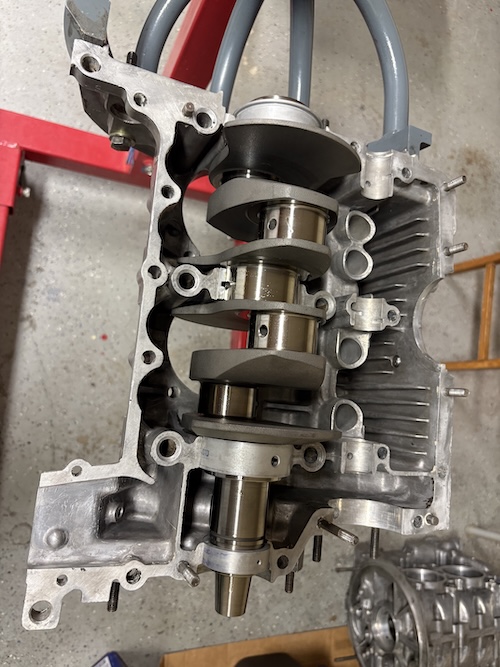
Posted by: friethmiller Jul 8 2026, 07:18 AM
Oil Pump Checks:
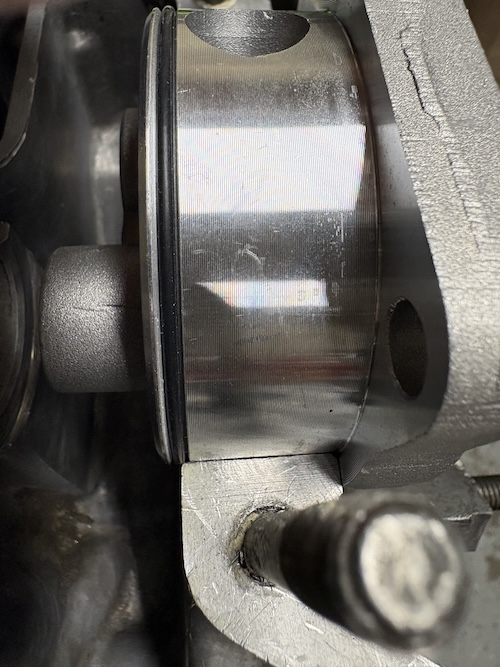
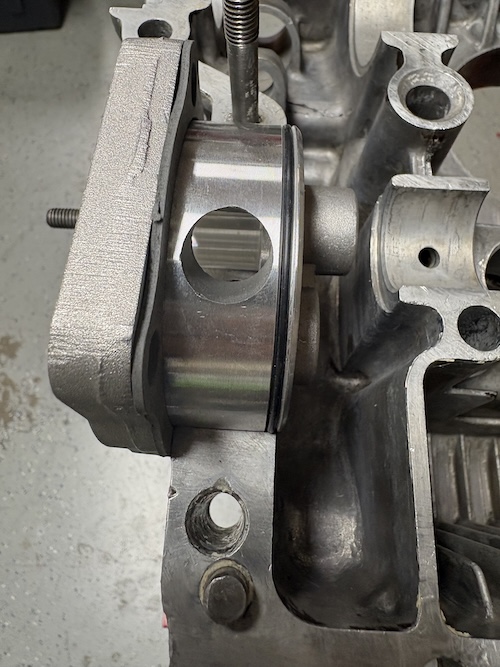
Measured my Schadek 30mm pump that I had used on this engine previously. After measuring it, I can feel a little better that my low pressure problem might have source from this housing. I couldn't get any measurement to hit the 70mm mark. My new, o-ringed, 30mm Schadek pump does. When I set the micrometer to 70mm, I can get the it to pass over the first pump without much of a problem. Whereas, I can't do the same with the new pump. 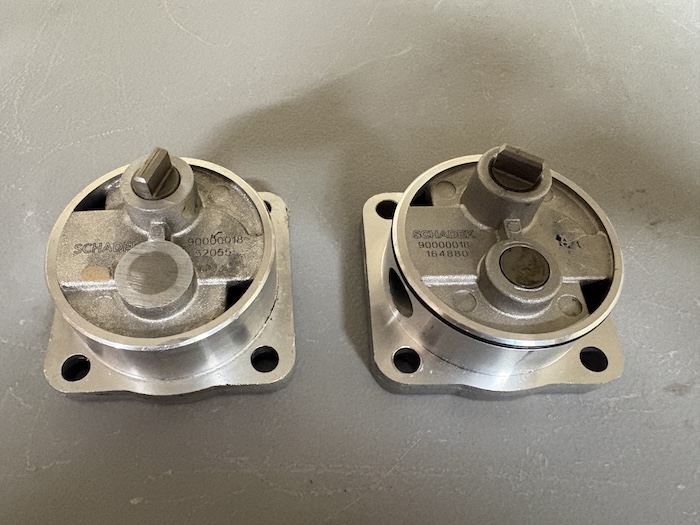
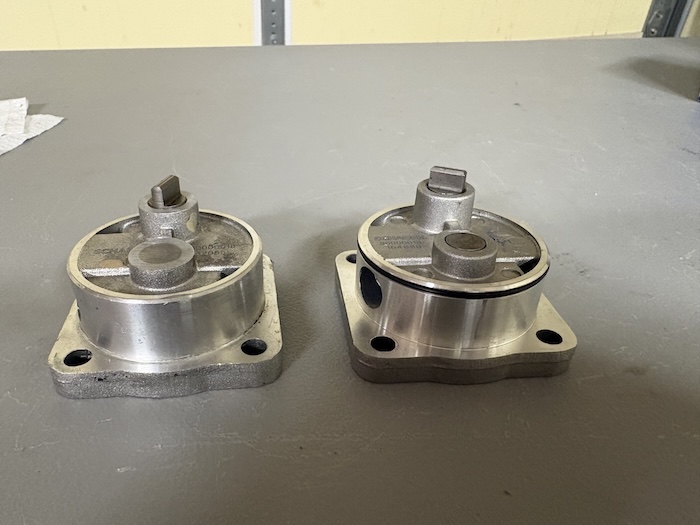
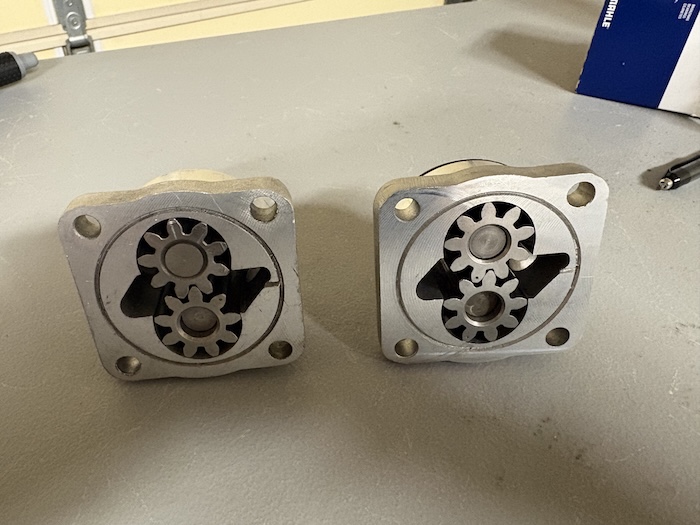
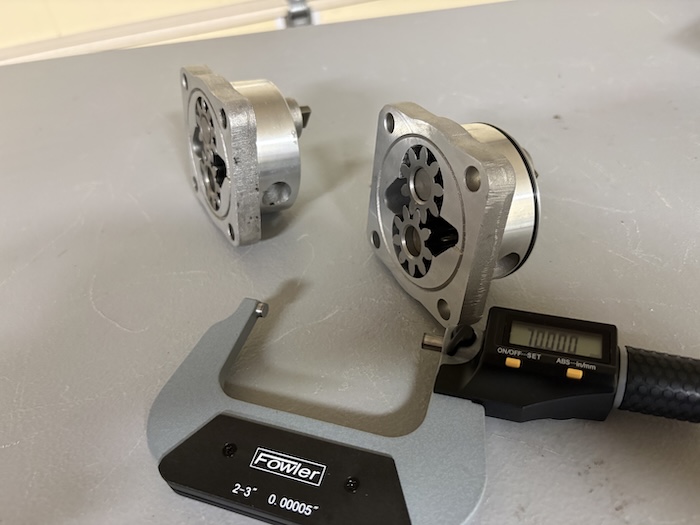
If i go with the new pump I'm going to need to source at little bit of a stand-off or a thicker gasket to pull the o-ring back into the bore just a bit. This is obviously not an issue in the Type 1 cases. No decisions have been made on any pump yet. Still measuring...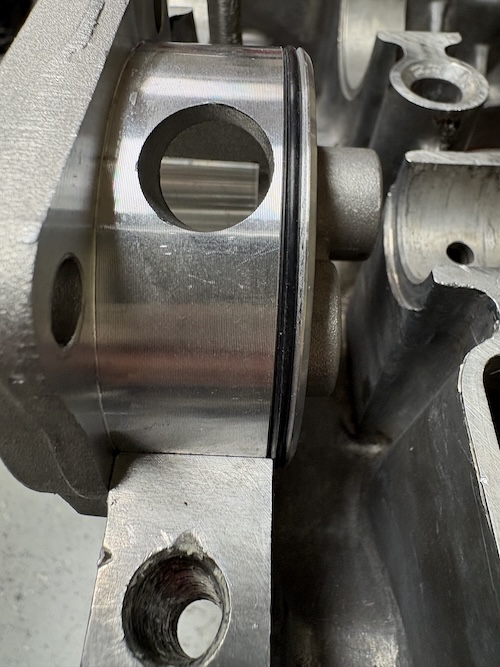
Posted by: friethmiller Jul 8 2026, 08:13 AM
Oil Pump Checks (Part2):
Pulled out the pump gaskets for the LE's new pump. Nice and thick! Boy, that makes that o-ring sit a lot better - when crushed it might be ok. 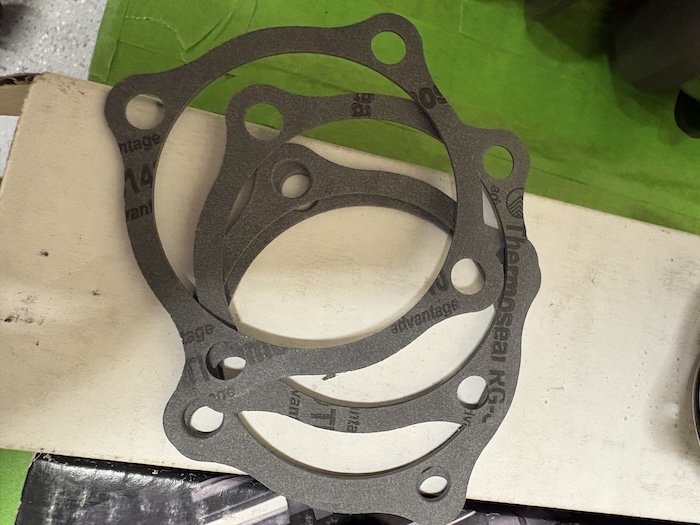
Posted by: friethmiller Jul 10 2026, 09:19 AM
More Measurement Data:
I've spent a lot of time measuring and re-measuring these cases to really dial-in on the numbers. Here's what I've got. Would welcome input from the experts / experienced.
W-Case Bearing Clearances:
Bearing #1 (Rear Main): 9 o'clock position is 0.003"; 12 o'clock (parting line) is 0.0025"
Bearing #2 : 9 o'clock position is 0.0015"; 12 o'clock position is 0.0025"
Bearing #3 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.002"
EC-Case Bearing Clearances:
Bearing #1 (Rear Main): 9 o'clock position is 0.002"; 12 o'clock (parting line) is 0.001"
Bearing #2 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.001"
Bearing #3 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.0015"
Question: Is either case usable as-is? The EC case probably needs to go get a clean 0.020 line bore - seem too tight on the parting line. What about the W-case? This has a fresh 0.020 line bore.
UPDATE: corrected decimal issue in measurements above
Posted by: Jack Standz Jul 10 2026, 12:16 PM
Oil Pump Checks (Part2):
Pulled out the pump gaskets for the LE's new pump. Nice and thick! Boy, that makes that o-ring sit a lot better - when crushed it might be ok.
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
Posted by: friethmiller Jul 10 2026, 12:27 PM
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
These came with a 26mm maxi-pump from CB Performance. I had already ordered these "thicker" gaskets from them before I found these in the LE's engine box. They'll probably be the same. I think they're arriving tomorrow. I can let you know.
Posted by: 930cabman Jul 11 2026, 05:25 AM
More Measurement Data:
I've spent a lot of time measuring and re-measuring these cases to really dial-in on the numbers. Here's what I've got. Would welcome input from the experts / experienced.
W-Case Bearing Clearances:
Bearing #1 (Rear Main): 9 o'clock position is 0.003"; 12 o'clock (parting line) is 0.0025"
Bearing #2 : 9 o'clock position is 0.0015"; 12 o'clock position is 0.0025"
Bearing #3 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.002"
EC-Case Bearing Clearances:
Bearing #1 (Rear Main): 9 o'clock position is 0.002"; 12 o'clock (parting line) is 0.001"
Bearing #2 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.001"
Bearing #3 : 9 o'clock position is 0.0025"; 12 o'clock position is 0.0015"
Question: Is either case usable as-is? The EC case probably needs to go get a clean 0.020 line bore - seem too tight on the parting line. What about the W-case? This has a fresh 0.020 line bore.
UPDATE: corrected decimal issue in measurements above
I am unsure exactly how close these measurement's can be. Not considering any lack of skills here, all of us are full aware of the talents Fred has displayed here. Please understand this.
What I am saying is a possible stack up of very minor inconsistencies. (tolerance stackup) Also, how close were these numbers when everything was brand new, possibly a very tight +/- tolerances for the case bores and the crank diameters. After 1/2 century I would probably run with these numbers. W case looks to have better numbers. I recently sent a 2.7 case to Ollies for inspection, they ended up line boring it due to the horizontal loads imposed on the case after many years of pounding. The bores become somewhat oval as you are seeing with your measurments here. Try to assemble the crank/bearings/case torqued and feel the resistance when turning the lubricated crank by hand.
I would go with this, your numbers look within a reasonable range
Posted by: friethmiller Jul 11 2026, 10:36 AM
@http://www.914world.com/bbs2/index.php?showuser=24877 - yeah, you’re probably right. Maybe it’s my measurements but if the fresh line bore on the W block was off, you’d think George at EMW would have told me. You know during the QA/QC checks. Or, maybe they don’t do that. Regardless, I’m going to have a conversation with him soon about this. I’m also going to wait on the case coming from Mr Heard. If his case checks out, I’ll be going that route. So, more to come on the case drama soon. Moving forward today with the rod clearance checks and crank assembly.
Oh, I appreciate your “talents” comment but I feel I’m only good at screwing it up 5 times before figuring it out. 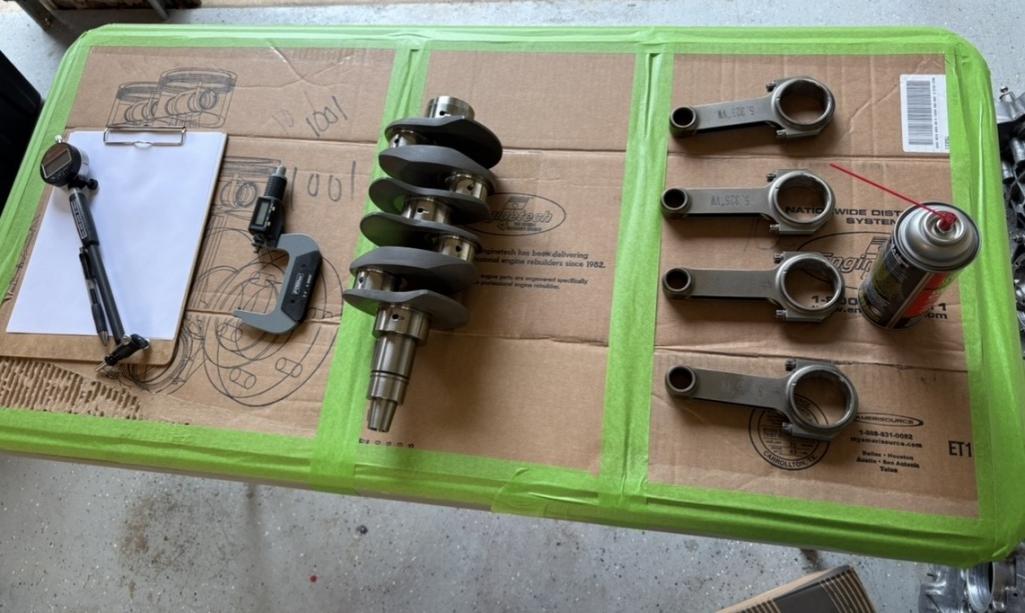
Posted by: 930cabman Jul 11 2026, 01:06 PM
I like Plasti Gage, it has worked well for me in the past and please trust I am far from an "engine builder", I have completed many air/water cooled rebuilds over the past 50+ years and have learned a thing or 2, but always check and double check everything and still check again.
Having the correct gauging tools is key here and I have never used the correct tools, but would like to assume the professionals have the right stuff and fully understand how to use them.
Great build 
Posted by: friethmiller Jul 11 2026, 02:59 PM
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
These came with a 26mm maxi-pump from CB Performance. I had already ordered these "thicker" gaskets from them before I found these in the LE's engine box. They'll probably be the same. I think they're arriving tomorrow. I can let you know.
Confirmed on that thicker oil pump gasket from CB Performance. You can buy it as a separate item.
Posted by: Robroe Jul 11 2026, 03:33 PM
Following you with great interest. I am also building a 2258 using Raby cam and Ham/Raby heads. I've disassembled a previously built but never run engine as it sat for 10 years. I just finished installing a new 30 mm pump from LN (Raby said it should work) and getting ready to install billet taco plate and sump. Then cylinders.
Posted by: friethmiller Jul 11 2026, 07:22 PM
I like Plasti Gage...
Me too! I think about it like this. If I miss-measure my crank's main journal with my micrometer (i.e. too tight), that will translate in a inaccurate zero setting with my bore gauge, and my clearance will be off. Plastigauge might seem crude but it doesn't have this problem. So, in regards to bearing #2, I'm absolutely going to use plasticgauge as an alternate measure. I just wish I could get it to work on the other journals.
 ...and let me know if you have a trick.
I'll pull the plastigauge out tomorrow and give it a go on #2. BTW, the material on this split bearing is different from the others in the set and is starting to show perpendicular scratches from all my bore gauge measurements. This could easily "tighten" the measurement here. And I am highly suspect of the 9-3 o'clock measure here. I'll snap a few pics of the results and report back.
Thanks for you input. Much appreciated!

Posted by: friethmiller Jul 11 2026, 07:23 PM
Following you with great interest. I am also building a 2258 using Raby cam and Ham/Raby heads. I've disassembled a previously built but never run engine as it sat for 10 years. I just finished installing a new 30 mm pump from LN (Raby said it should work) and getting ready to install billet taco plate and sump. Then cylinders.
Nice! Great to hear I'm not the only one building one at the moment. Best of luck! I hope it rips!!
Posted by: friethmiller Jul 11 2026, 08:08 PM
Moving Forward
While I wait for another case from Mark to arrive, I thought it best to move on with the crank to rod clearances. I measured the rod journals at a pretty consistent 1.9694". Zeroing the bore gauge to this, I got a very consistent .0015 - .002 on each rod. In fact, every rod measured .002 at the 12 o'clock position and .0015 everywhere else. You can see that I went "full clean" on these bearings/surfaces. I'm not planning on taking these bearing back out. 


With the case an unknown still, I can't install the #3 bearing and gears on the crank yet. So, instead, I gave everything a good "initial clean". Note the use of straight gears on this build. The machinist highly recommended I make this switch based on the HD double springs I'm running in my heads. The second pic shows me cleaning the cosmoline off of the cam gear. 

The next three pics show the 163/86b cam being installed with the gear in the padded vice. I'm assuming that I should be using the center (non-offset) washers for this gear. I will need to verify this tonight.


Final two photos show me lapping the oil pump cover on a piece of glass+sandpaper taped to the table. Despite the weird reflection in the photo - this thing was already flat. I must have done it last time. Better safe than sorry. 

I'm also working on several todos in the car's engine bay. For instance, I've already run a return line back to the tank and just need to pipe it up to the new fuel pressure regulator. This regulator is new and needs to be cleaned and installed, as well. I'll document some of this tomorrow. Till then.... Cheers!
Posted by: friethmiller Jul 11 2026, 08:42 PM
Yeah, I forgot about "Cam Degreeing". Damn! It just hit me with a type 4 ... this means I will need to mock-up the entire case/components, install the jugs, do this test, and then tear it all back down again to potentially use the offset cam gear washers. Nice! This should be exciting
Posted by: Jack Standz Jul 11 2026, 10:31 PM
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
These came with a 26mm maxi-pump from CB Performance. I had already ordered these "thicker" gaskets from them before I found these in the LE's engine box. They'll probably be the same. I think they're arriving tomorrow. I can let you know.
Confirmed on that thicker oil pump gasket from CB Performance. You can buy it as a separate item.
Thanks for checking Fred. Couldn't find it on their website, so was planning to go old skool and call them
.BTW when you degree the cam, it might be interesting if you could share where you set it and why please. However, kinda hard to get it "right" without a dyno. Looking forward to where you end up setting it either advanced or retarded. Of course it looks like you might be trying to just make sure it's straight up.
Posted by: friethmiller Jul 12 2026, 05:13 AM
Thanks for checking Fred. Couldn't find it on their website, so was planning to go old skool and call them
.Here it is:

It should say:
“Thicker than stock oil pump gasket, for use when installing Type-4 Oil Pumps.” in the description.
Posted by: friethmiller Jul 12 2026, 07:35 AM
Of course it looks like you might be trying to just make sure it's straight up.
Well, for now yes. I'm straight at 0 degrees. Depending on my measurements, I may need to advance or retard using the washers. That means my assembly of the case is without sealant till this is dialed-in.

Posted by: friethmiller Jul 12 2026, 09:26 AM
@http://www.914world.com/bbs2/index.php?showuser=24877 - Plasticgauge on the W-case. Brand new set of .50/STD bearings. Clearance on #2 bearing is confirm at .0015". Included a few pics.
Before & After Installing the crank with bearings (torque'd to 25lbs on the 6 case bolts). 

Measuring the gap:

Posted by: Ninja Jul 12 2026, 11:38 AM
Hi Fred,
Me thinks that's a great cam choice. It's pretty much what Raby developed and sold (maybe with a different LSA, not sure?).
Might want to run it a little advanced. We have two new ones (163/86b) in the boxes for upcoming projects, but was a little disappointed that we could only get them with 104 degrees lobe separation. But, understand that "custom" cams are months and months and months away.
Webcams makes good cams, so hoping you (and we) are happy with them!
All this to say that your LN lifters may be WebCam ones.
Right! I will find out. Here are the cards from both cams. 104 lc on both.
FYI, my intake/exhaust valves are 44/38 and my exhaust is a full 1 5/8” tangerine header + muffler.
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
These came with a 26mm maxi-pump from CB Performance. I had already ordered these "thicker" gaskets from them before I found these in the LE's engine box. They'll probably be the same. I think they're arriving tomorrow. I can let you know.
Confirmed on that thicker oil pump gasket from CB Performance. You can buy it as a separate item.
Thanks for checking Fred. Couldn't find it on their website, so was planning to go old skool and call them
.BTW when you degree the cam, it might be interesting if you could share where you set it and why please. However, kinda hard to get it "right" without a dyno. Looking forward to where you end up setting it either advanced or retarded. Of course it looks like you might be trying to just make sure it's straight up.

Jack speaks the truth!
It's super common to see cams degreed in with a bit of advance (for street use) or a bit of retard (high RPM race use).
But, it all depends on how the restrictions line up in the engine. How well the intake flows against how well the exhaust does.
The T4 is the single hardest "cam timing adjustment" engine I think I've seen yet.
Gota take the puppy completely apart to change anything!
I'm building a Toyota 3S-GTE Turbo MR2 engine with my son and I have adjustable gears. You put it together without the upper timing belt guard and you can alter cam timing in less than 5 minutes.
On that you wait till you're on the dyno before even worrying about cam timing.
I'd want LN, Raby, or Len Hoffman's take on cam timing for your set up if I could access that info.
Without a wizard's oversight, I'd put it in between 2-4 degrees advanced and run it (for street use).
You CAN degree a cam without pistons/rods/valve train, but you cannot find accurate TDC without at least one piston/rod/jug installed. You just take the cam timing reading off of a lifter.
That .050 timing measurement changes if you're taking the reading off of a lifter instead of a spring retainer. It will change depending on your rocker arm ratio.
I believe "off of the lifter" is more accurate than "off of the retainer".
Can you provide a close-up view of the main bearing bore surfaces on the line bored engine?
I'd like to see the surface machine marks.
I'm still having trouble with "how does a fresh line bore be non-concentric" as the machine itself cuts very accurate circles. They can easily be too large or too small (machinist error) but "out of round" seems impossible without a severely worn-out machine.
I use Plasti-Gauge on all of my builds as a final check. It's a verification tool after all the actual measurement are done. Yours looks great!
Plasti-Gauge shrinks with age! If it is 6 months old, it's GONE in my book.
I always buy new from someone like Summit as I'm hoping to get the newest stuff possible.
Believe what you measure OVER what Plasti-guage shows.
Posted by: 930cabman Jul 12 2026, 01:16 PM
@http://www.914world.com/bbs2/index.php?showuser=24877 - Plasticgauge on the W-case. Brand new set of .50/STD bearings. Clearance on #2 bearing is confirm at .0015". Included a few pics.
Before & After Installing the crank with bearings (torque'd to 25lbs on the 6 case bolts).
Measuring the gap:
Lookin great, and no, I wish there was a way to check the other main bearing journals with Plasti Gage. Rod bearing clearances a yes
Can we assume all the main bearing bores and the same size and in line?
Posted by: friethmiller Jul 12 2026, 07:51 PM
Can you provide a close-up view of the main bearing bore surfaces on the line bored engine?
I'd like to see the surface machine marks.
I'm still having trouble with "how does a fresh line bore be non-concentric" as the machine itself cuts very accurate circles. They can easily be too large or too small (machinist error) but "out of round" seems impossible without a severely worn-out machine.
Here's a few pics of the W case saddles. Any vertical marks are from me and my dial bore gauge.


If I use a metal ruler and sit it flush against the #2 saddle, you can see light under saddle #3. Saddle #1 looks pretty good. I'm not sure this ruler is good test but it doesn't lay flat. I made sure not to use #4. Need to find a piece of aluminum bar or something.
First photo show the ruler flat across the #2 saddle, with the headlamp against #3. Second photo shows the gap. Third photo is of saddle #1, no light.


Again, I think I need a better, thicker straight edge.
Posted by: friethmiller Jul 12 2026, 08:13 PM
Ok, I reassembled the W case again without bearings. I measured the 1-3 saddles for the 400th time - but this time in metric
Reminder: A standard case saddle is 70.0mm and a case with 0.50mm line bore should be 70.5mm +/- .02mm.
W-Case Saddle Measurements:
Saddle #1 : 9 o'clock position is 70.55mm; 12 o'clock (parting line) is 70.55mm
Saddle #2 : 9 o'clock position is 70.53mm; 12 o'clock position is 70.54mm
Saddle #3 : 9 o'clock position is 70.53mm; 12 o'clock position is 70.50mm
I've been "over-bored" This is a worst "case" scenario! Inadequate bearing-crush. Not good.
Rant: Why the hell don't they make enough type 4 bearings? And how about making some +/- bearings for custom fitting an engine for the above scenario?. There's no boring past .50mm mark.
Posted by: Jack Standz Jul 12 2026, 11:23 PM
Hi Fred,
Me thinks that's a great cam choice. It's pretty much what Raby developed and sold (maybe with a different LSA, not sure?).
Might want to run it a little advanced. We have two new ones (163/86b) in the boxes for upcoming projects, but was a little disappointed that we could only get them with 104 degrees lobe separation. But, understand that "custom" cams are months and months and months away.
Webcams makes good cams, so hoping you (and we) are happy with them!
All this to say that your LN lifters may be WebCam ones.
Right! I will find out. Here are the cards from both cams. 104 lc on both.
FYI, my intake/exhaust valves are 44/38 and my exhaust is a full 1 5/8” tangerine header + muffler.
Fred,
Where did you get these thick gaskets? They look like just what we need for some o-ringed oil pumps/projects.
These came with a 26mm maxi-pump from CB Performance. I had already ordered these "thicker" gaskets from them before I found these in the LE's engine box. They'll probably be the same. I think they're arriving tomorrow. I can let you know.
Confirmed on that thicker oil pump gasket from CB Performance. You can buy it as a separate item.
Thanks for checking Fred. Couldn't find it on their website, so was planning to go old skool and call them
.BTW when you degree the cam, it might be interesting if you could share where you set it and why please. However, kinda hard to get it "right" without a dyno. Looking forward to where you end up setting it either advanced or retarded. Of course it looks like you might be trying to just make sure it's straight up.
Jack speaks the truth!
It's super common to see cams degreed in with a bit of advance (for street use) or a bit of retard (high RPM race use).
But, it all depends on how the restrictions line up in the engine. How well the intake flows against how well the exhaust does.
The T4 is the single hardest "cam timing adjustment" engine I think I've seen yet.
Gota take the puppy completely apart to change anything!
I'm building a Toyota 3S-GTE Turbo MR2 engine with my son and I have adjustable gears. You put it together without the upper timing belt guard and you can alter cam timing in less than 5 minutes.
On that you wait till you're on the dyno before even worrying about cam timing.
I'd want LN, Raby, or Len Hoffman's take on cam timing for your set up if I could access that info.
Without a wizard's oversight, I'd put it in between 2-4 degrees advanced and run it (for street use).
You CAN degree a cam without pistons/rods/valve train, but you cannot find accurate TDC without at least one piston/rod/jug installed. You just take the cam timing reading off of a lifter.
That .050 timing measurement changes if you're taking the reading off of a lifter instead of a spring retainer. It will change depending on your rocker arm ratio.
I believe "off of the lifter" is more accurate than "off of the retainer".
Can you provide a close-up view of the main bearing bore surfaces on the line bored engine?
I'd like to see the surface machine marks.
I'm still having trouble with "how does a fresh line bore be non-concentric" as the machine itself cuts very accurate circles. They can easily be too large or too small (machinist error) but "out of round" seems impossible without a severely worn-out machine.
I use Plasti-Gauge on all of my builds as a final check. It's a verification tool after all the actual measurement are done. Yours looks great!
Plasti-Gauge shrinks with age! If it is 6 months old, it's GONE in my book.
I always buy new from someone like Summit as I'm hoping to get the newest stuff possible.
Believe what you measure OVER what Plasti-guage shows.
Hi Rick,
Yeah, for those that are adjusting cam timing, it can be a real, PIA. Depending on your setup, you may get away with pulling the oil pump and adjusting the fasteners on the cam gear through there. That's our plan.
But not gonna run the motor on a dyno. Mockup like Fred is doing. Best guess parallels what you said about 2 to 4 degrees is probably good enough. However, gonna start with a baseline measurement of where the cam is per the cam card versus where the cam was ground when using a standard non-adjustable gear. Curious to see what we find and how it works out. Really and honestly don't know what we will find or where we will set the cam timing. At least not yet.
Getting back to the comments about Raby, LN and cam timing and LSA. The 104 Fred and we are gonna run will probably be OK. It seems that Raby and LN only make changes/fine tuning of the LSA for those running their motors at significantly different altitudes.
Posted by: friethmiller Jul 13 2026, 07:52 AM
Fuel Regulator:
I needed to mount the new PMO fuel regulator at carburetor height in the engine bay. With the way the fuel lines are already routed, this meant installing it somewhere on the back wall of the engine bay. Unfortunately, the center position is occupied by the TR oil catch can/breather. The supplied mounting plate was good but wasn't the right size for the mounting location. So, I set out to fabricate a mount of my own. Note the diagram in the first pic. The return line output is on top then input with two outlets on the face that go to the carbs. 

From the cut out that I had mocked up in the engine bay, I went out to the shed and found some scrap 16 gauge sheet metal. After cutting the shape, I then drilled the necessary holes, painted it, and then mounted the regulator.

I then mounted the entire assembly against the back wall. You may notice that I did do a little bending of the mount itself. I needed to account for the angle differences of the bolt location on the back wall. I also bent the mount below this point (horizontally) to allow the regulator to set more upright. The one problem with the mount as I found out was the interference with the hose clamps. I need smaller clamps for the 8mm hose for sure but I may remove and cut the mount a bit to alleviate the problem. Not bad though. 

Final photos show the routing of the lines and the lower firewall. With the added return line and my A/C wire routing + new bus bar, things sure have gotten congested in this area. I still need to clean up the hoses and wire with a few good zip-ties. Again, not too bad.

Posted by: Ninja Jul 13 2026, 08:08 AM
WOW! those machine marks don't look even...
Doesn't look like they dressed the edges either!
Your ruler test looks like crap!
How can they machine it like that?
There is a "fix"...
You won't like it.
Machine both sides of the parting surface on the cases .010.
Now you have to line bore EVERYTHING!
You will need a really competent machine shop at that point.
Easier to find another case.
Posted by: Ninja Jul 13 2026, 10:43 AM
Heads up!
Checking line bore without the cases bolted up is the INCORRECT way to do it.
Cases should be torqued up!
However, I just checked this on my torn apart 2.0l GA cases I mentioned exactly like you did and mine seem straight...
I used an 18" Mitutoya machinist straight edge that has been checked for accuracy with a 36" Starrett straight edge.
The light emission under each journal were identical.
Posted by: 930cabman Jul 14 2026, 01:00 PM
WOW! those machine marks don't look even...
Doesn't look like they dressed the edges either!
Your ruler test looks like crap!
How can they machine it like that?
There is a "fix"...
You won't like it.
Machine both sides of the parting surface on the cases .010.
Now you have to line bore EVERYTHING!
You will need a really competent machine shop at that point.
Easier to find another case.
perhaps a call to Ollies is in order
Posted by: friethmiller Jul 14 2026, 01:23 PM
perhaps a call to Ollies is in order
Ollies in AZ? Just talked with them. They don't do VW line-bores. Any other recommendations? Anyone have a good shop that does Type 4 line bores?
I've emailed and left messages at Headflow Masters and Brother's Machine both in CA. No response [yet]. Just talked with George at LN Engineering. He said they are 2-3 months out (at best) on providing that service.
Don't we have some East Coast options? I'm about done with CA
Posted by: 930cabman Jul 14 2026, 07:25 PM
Wish I knew of a reputable VW/Porsche engine machine shop
several years ago I had my local machinist turn a "case gauge" simply a straight shaft with a thou or so undersize from the main bearing bores. The hope was to use this to inspect the several T4 cases I have laying around. Well life got in the way and this is still unproven. works on paper, in practice has yet to be proved
My default gage is having the assembly torqued and the "feel" of a lightly oiled crank in new bearings
Posted by: friethmiller Jul 14 2026, 07:51 PM
I hear ya there. When I torqued the crank in my EC block last week it wasn't binding but I could tell it was just a bit firm. Not saying I've got "the touch" but I think over time I'm beginning to learn the feel. What that means as far a .001s? No clue  Saying sh!t like this guarantees a post from @http://www.914world.com/bbs2/index.php?showuser=29004
Posted by: 930cabman Jul 15 2026, 04:55 AM
I hear ya there. When I torqued the crank in my EC block last week it wasn't binding but I could tell it was just a bit firm. Not saying I've got "the touch" but I think over time I'm beginning to learn the feel. What that means as far a .001s? No clue
Saying sh!t like this guarantees a post from @http://www.914world.com/bbs2/index.php?showuser=29004 When you did the crank "feel test" were you using the flywheel or the fan?
No binding is a good thing
Posted by: friethmiller Jul 15 2026, 05:36 AM
I hear ya there. When I torqued the crank in my EC block last week it wasn't binding but I could tell it was just a bit firm. Not saying I've got "the touch" but I think over time I'm beginning to learn the feel. What that means as far a .001s? No clue
Saying sh!t like this guarantees a post from @http://www.914world.com/bbs2/index.php?showuser=29004 When you did the crank "feel test" were you using the flywheel or the fan?
No binding is a good thing
I was turning the hub placed on the nose of the crank with one hand.
Posted by: 930cabman Jul 15 2026, 09:03 AM
I hear ya there. When I torqued the crank in my EC block last week it wasn't binding but I could tell it was just a bit firm. Not saying I've got "the touch" but I think over time I'm beginning to learn the feel. What that means as far a .001s? No clue
Saying sh!t like this guarantees a post from @http://www.914world.com/bbs2/index.php?showuser=29004 When you did the crank "feel test" were you using the flywheel or the fan?
No binding is a good thing
I was turning the hub placed on the nose of the crank with one hand.
Given the information available I would give this a go
Posted by: friethmiller Jul 15 2026, 12:36 PM
Given the information available I would give this a go
I would... but I saw the condition of the bearings coming out of this case 18 months ago (below)
The engine had less than 5,000 miles on it. I'm erroring on the side of caution here. UPDATE: Today the W case shipped back to EMW and the EC case went to Brother's VW Machine. Both cases will arrive in CA on Monday. Here's to getting something back that is in spec.

Posted by: 930cabman Jul 15 2026, 01:01 PM
Given the information available I would give this a go
I would... but I saw the condition of the bearings coming out of this case 18 months ago (below)
The engine had less than 5,000 miles on it. I'm erroring on the side of caution here. UPDATE: Today the W case shipped back to EMW and the EC case went to Brother's VW Machine. Both cases will arrive in CA on Monday. Here's to getting something back that is in spec.
Question for the brain trust:
Would you say these bearings suffered from ill fitting or contamination?
and how much did they suffer? was the oil pressure acceptable? engine runing ok?
Posted by: Ninja Jul 15 2026, 01:26 PM
Ill fitting!
But I'd want to see all of the bearings in order with correct clocking to look across the entire set.
The picture at 5K looks like a "COME BACK" to me.
Posted by: friethmiller Jul 15 2026, 01:37 PM
Note the backs of these same #2 bearings. Note: these are old pics that Rick has already seen.
Posted by: 930cabman Jul 16 2026, 04:50 AM
Once again, I am not a "real" engine builder, but if I had to guess my bet would be contamination. Bearing surface does not appear wiped out. How was the engine running prior to removal?
Hoping to see more input here
Posted by: friethmiller Jul 16 2026, 06:33 AM
Once again, I am not a "real" engine builder, but if I had to guess my bet would be contamination. Bearing surface does not appear wiped out. How was the engine running prior to removal?
Hoping to see more input here
It ran but there were multiple issues at play here. The top end of the motor was built incorrectly. The cam’s thrust bearing surface was flaking off and one of the pushrods had mushroomed and was causing damage to the top of the lifter. The reason I pulled the engine was due to metal in the oil. So, while I think the bearing clearances weren’t good, the top end was beginning to come apart and contaminated the oil.
 .


Posted by: friethmiller Jul 16 2026, 08:33 AM
All this is in the past, though. I'm looking forward to getting the case back and starting to build the engine up correctly with a little forum assistance.
Posted by: 930cabman Jul 16 2026, 12:22 PM
All this is in the past, though. I'm looking forward to getting the case back and starting to build the engine up correctly with a little forum assistance.
In the past yes, but what can we learn from this mess?
My $5.00 would go with contamination from pushrods, improper thrust, .... falling apart
Possible the case is fine
Posted by: friethmiller Jul 16 2026, 01:26 PM
All this is in the past, though. I'm looking forward to getting the case back and starting to build the engine up correctly with a little forum assistance.
In the past yes, but what can we learn from this mess?
My $5.00 would go with contamination from pushrods, improper thrust, .... falling apart
Possible the case is fine
Understood. You're probably right. I'm sure the case is fine but I won't rush the process this time. When my case returns and checks out, I will proceed. The lesson learned here is don't trust a lot of these "so called" professionals. You must verify measurements, check clearances, and make sure everything is right. I'm not guilt free here, either. I've learned a lot of hard lessons a long the way.
Let me bring everyone up to speed on the history of this engine (it isn't pretty).
1) 2019: Engine goes to Fat/Rimco for machine work - decided to have them build the long block (during Covid).
2) 2021: Put my new engine on test stand. Break-in engine - no issues.
3) Run engine a 2nd time to verify timing adjustments. 5mins into test run, engine begins bellowing smoke bad.
4) Call Rimco. Pissed. I am told to install into car and drive it.
5) Drive car with new engine - continues to blow smoke, gets worse and then seizes.
6) Tow car back home, call Rimco. I am told that since they only built a long-block they aren't at fault here. I'm pissed, tell them what I think of them (and their mothers).
7) Tear-down engine myself, find a metal ball of shavings in #2 main oiling hole in crank blocking oil passage. Really pissed off!
8) 2022: Decide to build it back myself... pay more money and get crank ground and purchase new 96mm cylinders, bearings, etc. Rebuild motor myself but don’t make any major changes – assume value-train is correct.
9) Install engine and it runs great for 2 years not a ton of power but it runs. All is good till metal shows up in oil.
10) 2023: Fat/Rimco goes out of business... because they absolutely sucked and possibly due, in part, to my "negative word of mouth" campaign

11) 2024: Tear down engine again. Realize that Rimco’s deck height measures over .080. Also, determined that I used the wrong ring set for the low profile KB pistons (needed to be pinned
). The loose oil rings trashed another set of 96mm cylinders. Find cam thrust bearing damage, and push-rod and lifter damage.12) 2025: Send parts to Automotive Machine & Supply to get case looked at and parts modified and balanced.
13) Wait 18 months patiently - finally tell owner that I have a spare case (since that was the hold-up).

14) 2026: Pick-up parts and start taking measurements – realize cases are not within spec.
Posted by: 930cabman Jul 16 2026, 05:58 PM
Whoa, quite the timeline. The learning experience is probably the only positive part that can be taken from this mess.
Myself I would rather attempt mostly any task and screw it up a couple times instead of having a professional screw it up.
I once heard a theory regarding any sort of work (ditch diggers, surgeons, lawyers, you name it): 1/3 of the professionals are really good , know their stuff and are standup guys, another 1/3 have their hearts in the right place but just can't get it right and the remaining 1/3 just don't have a clue. I'll bet it's a close approximation
Keep the course and yes there are nightmares, unfortunately with this engine you have lived it
Posted by: friethmiller Jul 17 2026, 10:56 AM
@http://www.914world.com/bbs2/index.php?showuser=24877 - so true! Thanks for your input/wisdom - and others as well. The downtime for the cases will not go to waste. Aside from working on the LE, I'm already "hot" on other tasks that need to be done for this car. You've already seen the new fuel return line and fuel regulator but I'm also working on installing TR's side-shift and external oil cooler kits. @http://www.914world.com/bbs2/index.php?showuser=29004 will be happy to hear I'm also installing dual CHT sensors and an AFR, which connects nicely to the TR exhaust.
Posted by: Ninja Jul 17 2026, 12:19 PM
Awesome!
Chris's exhaust is exemplary!
Bit pricey but bad to the bone!
Ninja approved!
Posted by: friethmiller Jul 17 2026, 01:24 PM
Do I have to run the AFR gauge into the main cabin? This cable is thick. Would it be sufficient just run it into the engine bay and put the gauge there? I know it's not a gauge that you don't need all the time. Opinions welcome?
Posted by: Ninja Jul 17 2026, 02:23 PM
I'd watch that gauge more than anything else but the tach...
INSIDE the car
Posted by: zig-n-zag Jul 17 2026, 05:02 PM
The “initial mock-up test fit” and “case gauge” comment triggered a memory on how I was told to determine if a case was still good or not.
Say you came across a used Type 4 engine for sale which was complete and still together. Check the 6 case bolts if they are still torqued to factory spec. If they are, then torque those case bolts to 30 ftlbs. The crank should still turn smoothly. Any binding means the case would need a line-bore.
If the nuts were loose, inspect the case saddles. The original machining marks should be visible. If not, then line-bore. Yes, you can check by installing a crank with bearings and do the 30lbs test, and it will probably pass. But if built, when the engine comes up to operating temperature, it may seize.
Posted by: 930cabman Jul 17 2026, 05:58 PM
Do I have to run the AFR gauge into the main cabin? This cable is thick. Would it be sufficient just run it into the engine bay and put the gauge there? I know it's not a gauge that you don't need all the time. Opinions welcome?
I purchased an Innovate LM 2 several years ago, just recently got it connected successfully (connected into the cabin), it is showing rich under 3k rpms telling me the idle circuit needs to be leaned out. In the past I have relied on the color of spark plugs for AFR. Has worked ok for me, but I am far from a dyed in the wool tuner, more like seat of the pants.
I like having a tube fed oil pressure gauge and a capillary tube temp gauge in the cabin. BUT, my builds are stock, nothing out of the ordinary. I'll bet cylinder head temps are also important
Posted by: Jack Standz Jul 17 2026, 07:39 PM
Do I have to run the AFR gauge into the main cabin? This cable is thick. Would it be sufficient just run it into the engine bay and put the gauge there? I know it's not a gauge that you don't need all the time. Opinions welcome?
Fred.
Are you messing with us?
Don't see how the gauge does you any good if you can't see it. So, yes in the main cabin where you can take note of AFRs under load, at different RPMs, WOT, going downhill, at cruise, etc. An AFR gauge really helps dial in carbs, idle jets, main jets, air correction, emulsion tubes, pump jets, venturis, etc.
With all the possible combinations of adjustments, it is an iterative process, so you'll want to note how your changes affect the AFRs. Then at some point you say things are "good enough", especially if you regularly run the car at sea level and at altitude. Until then, it's a gauge you're always watching.
Posted by: friethmiller Jul 17 2026, 08:45 PM
Yeah that doesn’t make sense for an AFR. Can’t really see back there while you’re driving. I was looking at the wrong end of the cable and thinking “how in the world am I going to get this huge connector through the firewall". Luckily the other end was much smaller. I’ve already routed it with the CHT wires up under the console. Next, I need to figure out exactly how/where I going to mount the gauges.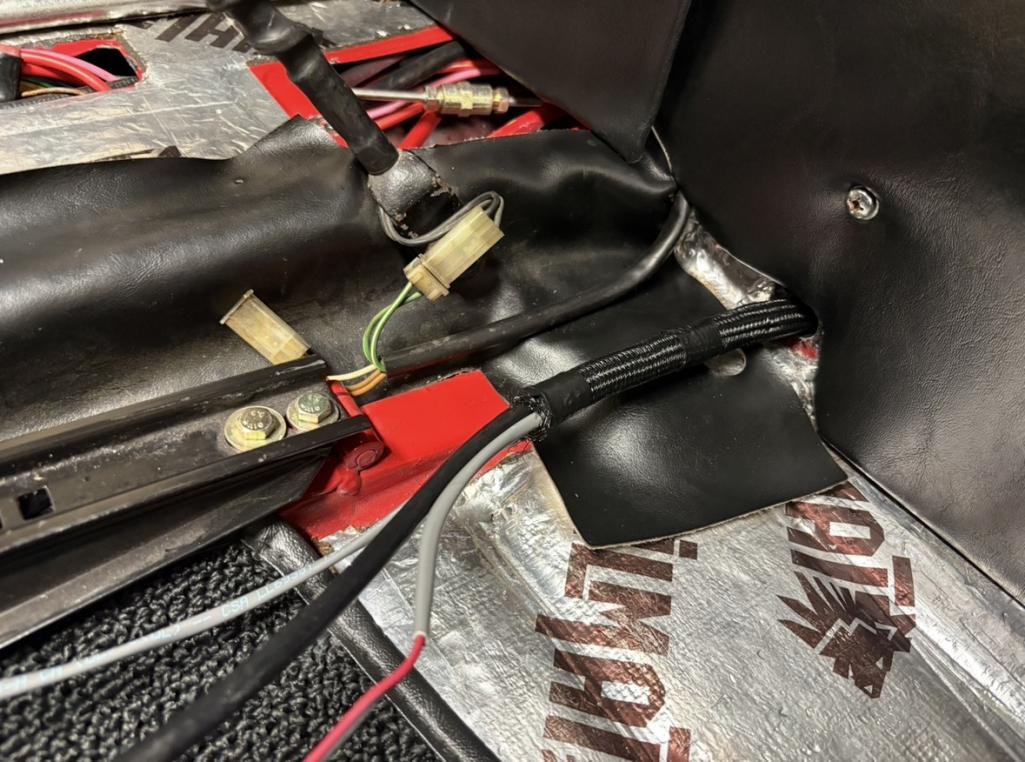
Posted by: friethmiller Aug 14 2026, 08:24 AM
Quick Update:
Brothers VW Machine in CA was able to verify and fix the problem. They lightly polish my new crankshaft to provide the correct clearances for my EC case. If you recall, the parting line oil clearances were the issue with this case. I will of course verify things again once it's back in the garage. The case, bearings, and crank will likely return the middle of next week. So, next weekend will be set aside for getting [re]started.
Posted by: friethmiller Aug 22 2026, 10:12 PM
Engine Assembly - Part 1 (8/22/2026):
With the case, crank, and bearings back from Brothers VW Machine, I quickly verified measurements and then completely rewashed the case halves to get ready for assembly. The guys had lightly ground my new crankshaft to provide a bit more oil clearance. I did have an issue with measuring the #2 main but I verified it was just my measurements of the crank journal OD and I verified it with some pastigauge.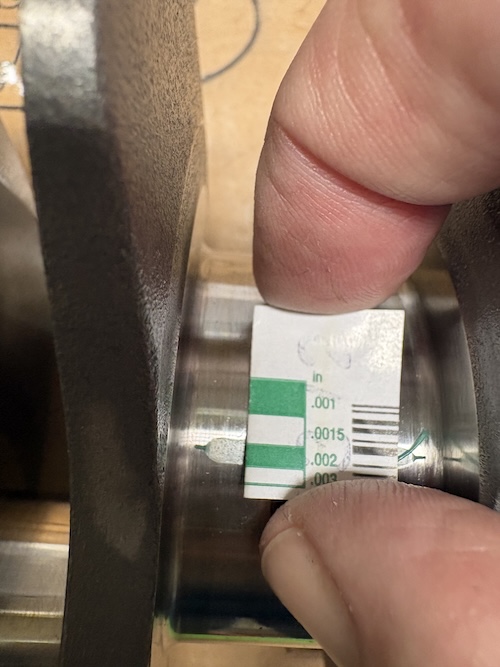
With everything cleaned, I set out to slide on the gears and test fit everything into the case. Even with the case torqued, everything felt good, no issues rotating the crank with one hand. I did trade out one of the thrust bearings on the cam. One half was too tight so I swapped it out with a spare. I am running a double thrust for this application, of course. 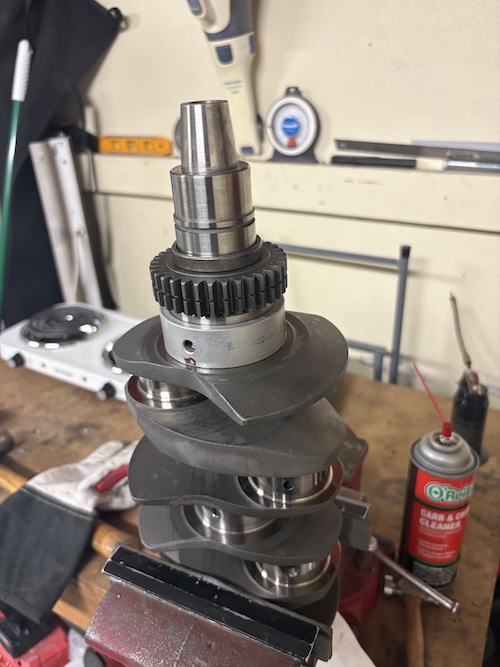
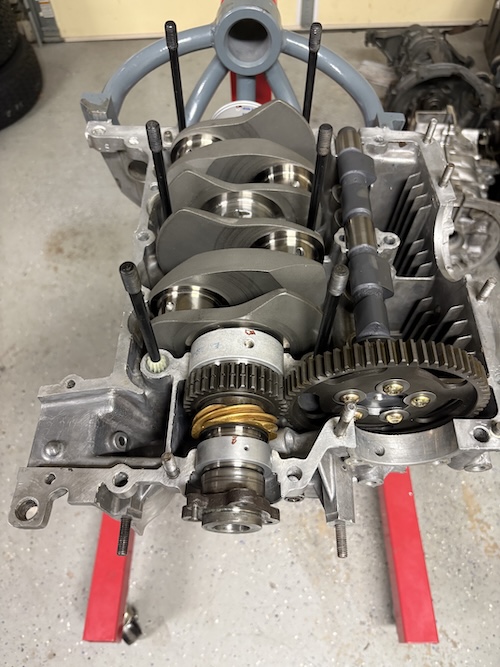
I then pulled everything back apart and cleaned and installed the rods that were already to go.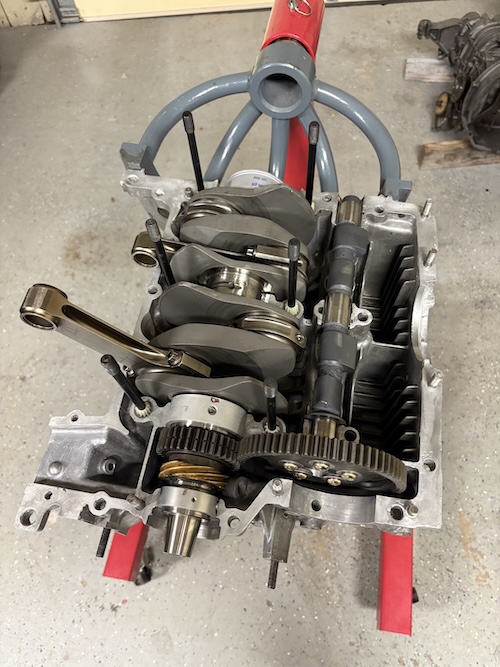
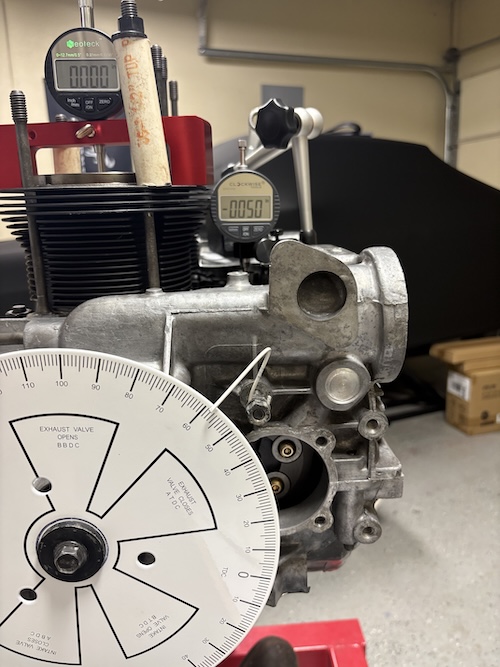
Again, the case was reassembled and torqued. This time I proceeded by installing all of the head studs using the permatex thread sealant. Next, I added pistons & cylinders for 1&2 (without rings) and got things ready for degreeing in the cam. The timing wheel I was using wasn't really made for VW engines and I had to remove the air/fan shroud studs to properly "clamp" the wheel with the crank bolt. I also used a short section of a clothes hanger to act as a pointer. Pretty easy to do.
So after watching about 6 different Cam Degreeing videos, I felt like I might actually understand what I had to do and why I was taking these measurements.
First step of the process was finding true TDC, which was roughed in by eye and then adjusted by going .050 in either direction to verify my zero (TDC). 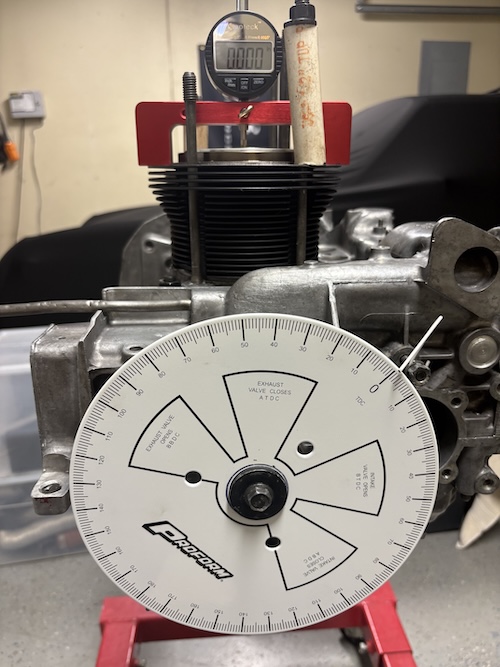
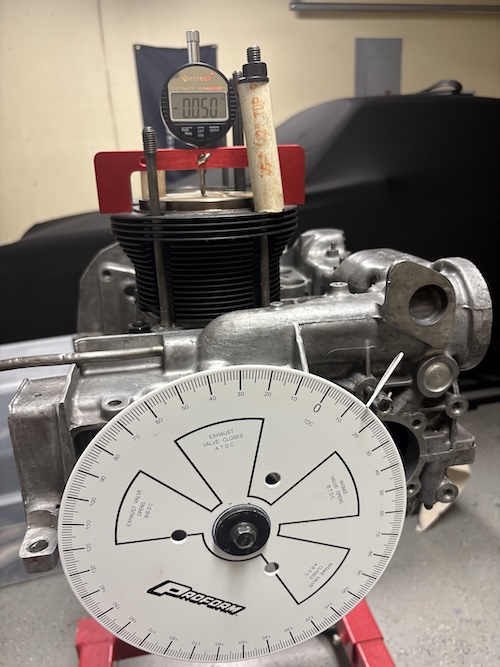
With this initial task complete, I then moved over to setting up something to measure intake lift using a installed lifter. To set this up, I cut a piece of 16 gauge sheet metal to allow my magnetic base to clamp down to something. I used the 10mm studs on the side of the case that normally secure the thermostat. The next job to do was to measure max intake lift. And here's where things got off track a bit for me. I was getting lift measurements that were low and I couldn't figure out why initially. It turned out the two small bolts that my base was secured to were not enough to prevent the entire stand from moving during this measurement. I think If I had secured the base using a third bolt somewhere, I probably wouldn't have had the issue. To get past the problem, I simply jammed a box wrench between the base on the engine case to prevent things from moving. Another issue was the reach of the dial gauge. It wasn't long enough to reach far enough into the lifter bore to take any measurements at all. There just too much stuff in the way. I got around this problem by stacking a second lifter in the bore. This worked great for me but I'm sure a longer pointer would be available for purchase for the bore gauge. With all the bandaid fixes deployed, I was finally able to get a measurement of .3895 which is just shy of .390 that, when multiplied by the 1.3 rocker arm ratio matches the targeted .507 of valve lift. 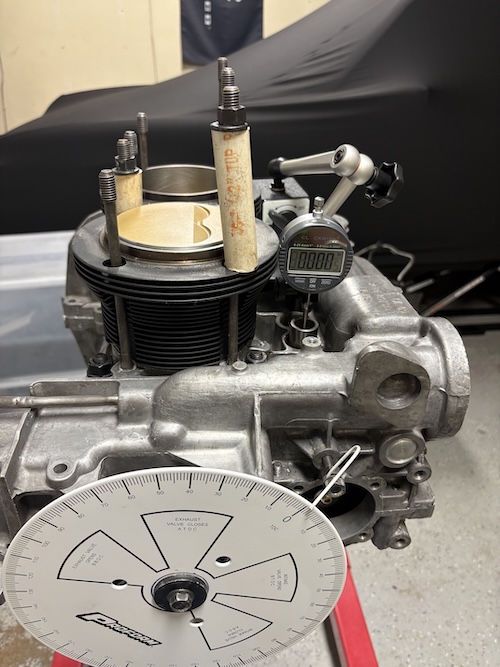
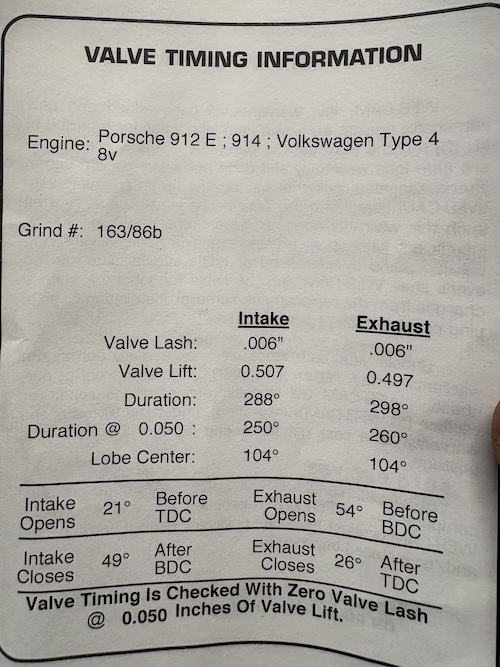
Once you have max valve lift, you can then find your lobe center. This is where I zeroed the dial gauge at max lift and then rotated the cam wheel .050" in either direction taking the degree measurements.
For this I got 145 and 59 degrees. Adding them together, I got 204 degrees and then dividing this number by 2 and got an intake lobe center of 102 degrees. I know that if the number is less than the expected value of 104 degrees, the cam is "advanced" by 2 degrees. I think 2-4 degrees would be ideal for street use and might be good to go here. More measuring coming soon. Cheers! 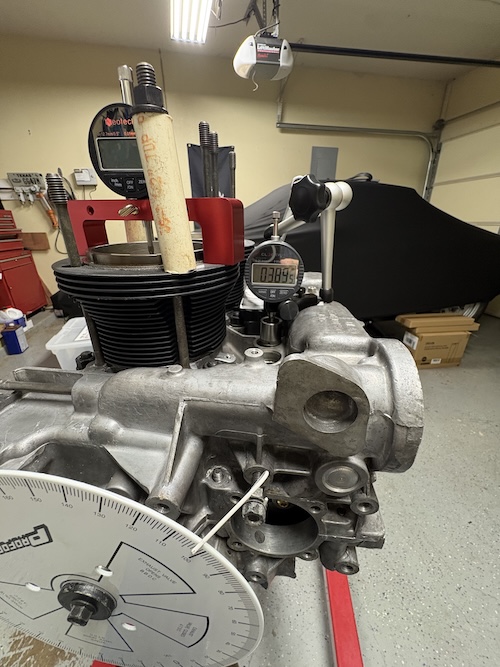
Posted by: seanpaulmc Aug 23 2026, 05:44 AM
You’ll be driving to Okteenerfest, Fred! 
Posted by: 930cabman Aug 23 2026, 06:06 AM
lookin good, have you torqued the case together and checked the crank "feel"
Posted by: friethmiller Aug 23 2026, 06:24 AM
Yeah, the crank feels good/rotates without any binding with the case bolts torqued. I still need to do more cam measurements this morning but will be splitting the case to locktite the cam bolts, insert the o-ringed oil pump, etc. before beginning the process of sealing the case together.
Posted by: friethmiller Aug 23 2026, 07:35 AM
You’ll be driving to Okteenerfest, Fred!
Wouldn't that be wonderful!
Let's call it a "long shot", for now.
Posted by: Ninja Aug 23 2026, 08:05 AM
That's just BS!!!!!
Fred only has to do it ONCE!!!!
Not fair!!!!
Looks GREAT!
I'd leave it where it is...
Posted by: friethmiller Aug 23 2026, 08:46 AM
Ok, intake duration measured .05 open at 23 degrees before TDC and closes (0.05) after BDC at 47 degrees. That’s (23+47+180)/2 = 250 degrees of duration. That’s spot on! Exhaust is next.
Posted by: friethmiller Aug 23 2026, 08:53 AM
@http://www.914world.com/bbs2/index.php?showuser=4366 Standz, note I’m using a 9inch wheel here. Anything larger would probably get in the way of easily replacing the offset washers on the cam. I’m good with splitting the case again for the oil pump install but with a normal pump you could just install it and move on.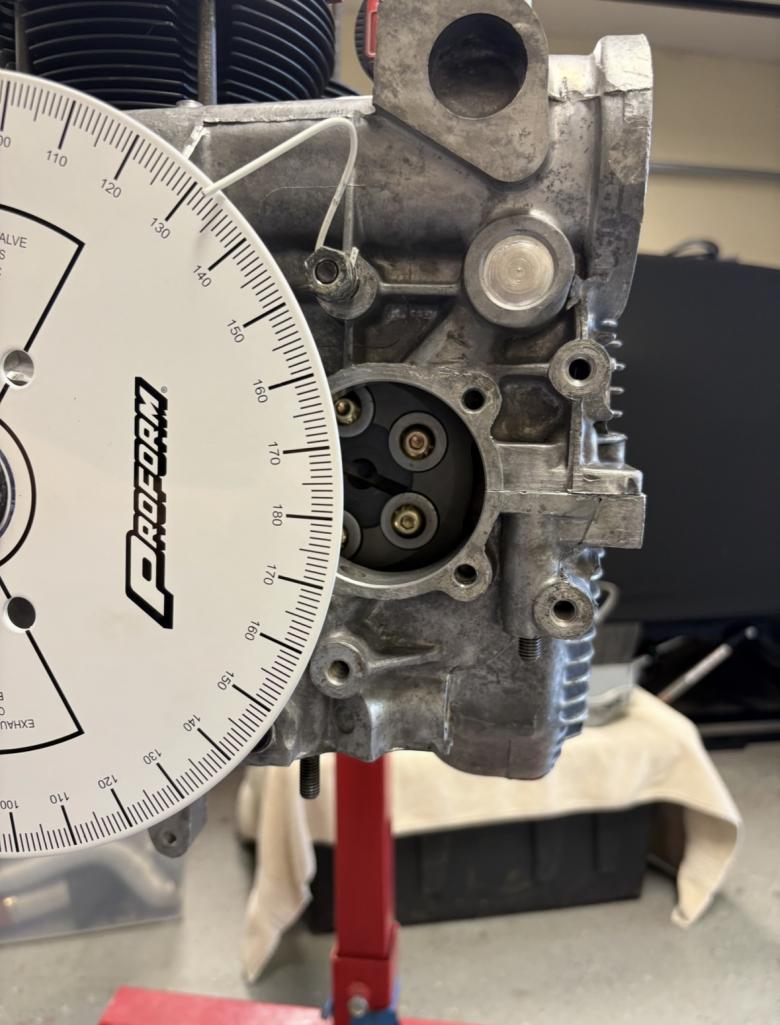
Posted by: 930cabman Aug 23 2026, 09:33 AM
I would take my time, check and double check everything
Go Fred go
great project, thanks for posting
Posted by: friethmiller Aug 23 2026, 09:36 AM
Exhaust:
Calculated max lift of .496
Lobe center: 108 degrees
Duration: 262 degrees
That’s an ICL of 105.5 ATDC and an ECL of 103.5 BTDC
LSA = (105.5 + 103.5)/2 =104.5
Posted by: friethmiller Aug 24 2026, 08:59 AM
Building up the Short Block (8/23/2026):
First pic shows the base I made for my dial gauge stand. At 16 gauge, it just wasn't thick enough and it needed a third point to really lock it down and keep it from moving ever so slightly.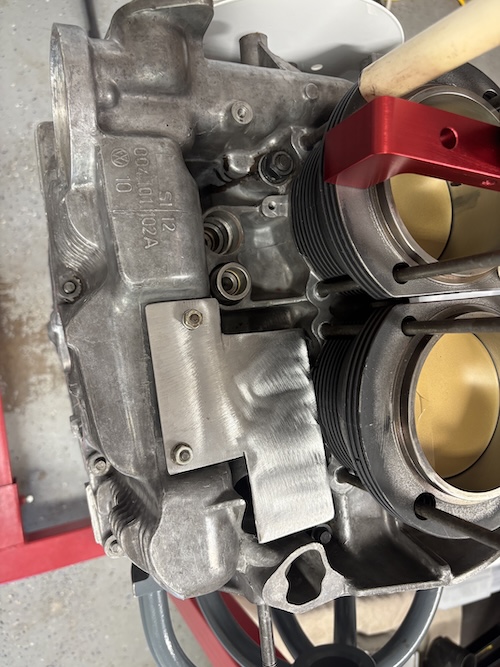
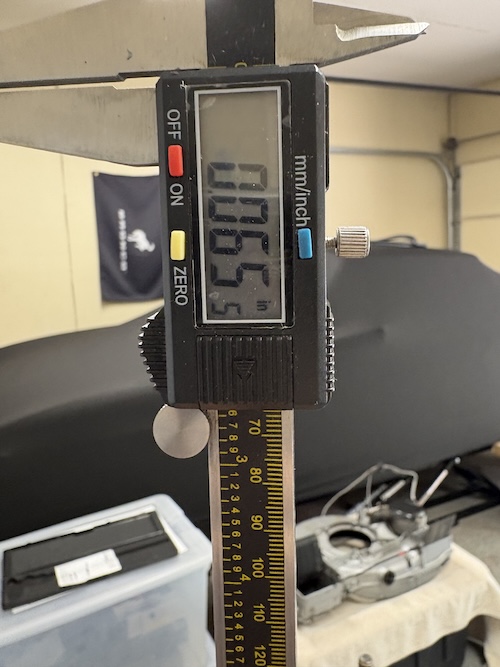
Before tearing everything down, I took the opportunity to get a rough sense of the shims I would need to order to set the proper deck height. You can see how a longer 78mm crank pushes the piston above the top of the cylinder. I'm basically plus .065.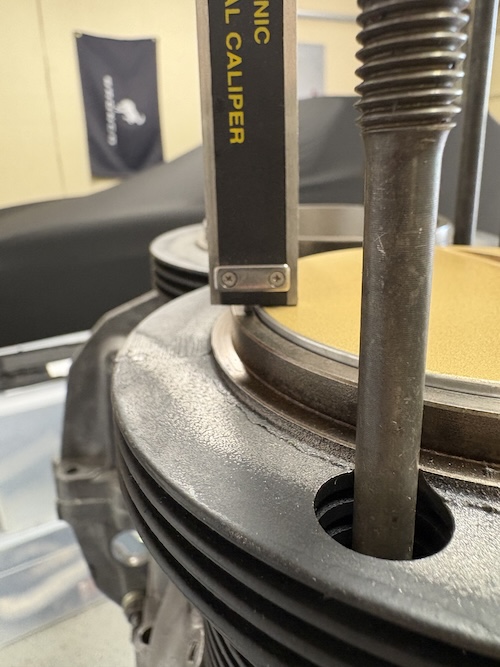
With the cam properly degreed, it was time to prep everything for the final install of the case halves. I had to loctite in the cam bolts, test fit the oil pump, insert/index the distributor, lubricate everything that needed oiled, and clean-up mating surfaces. Here's a few photos.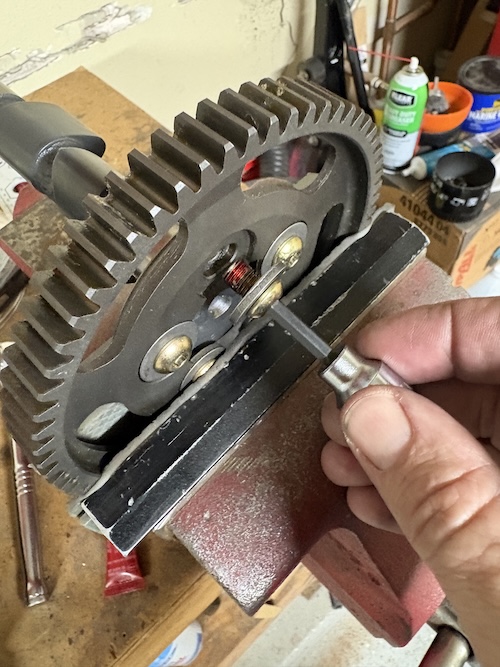
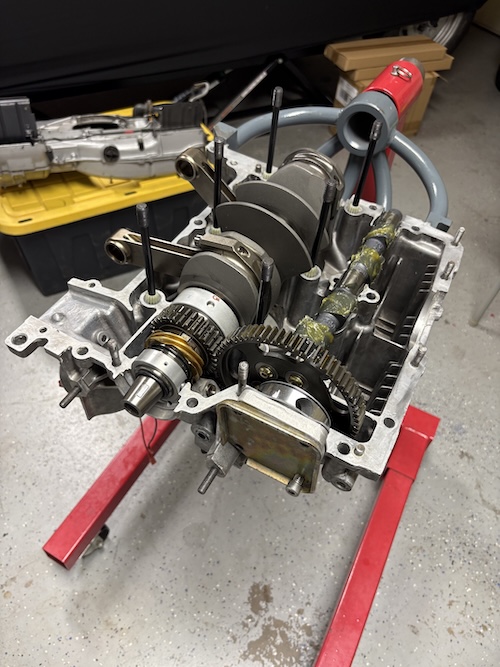
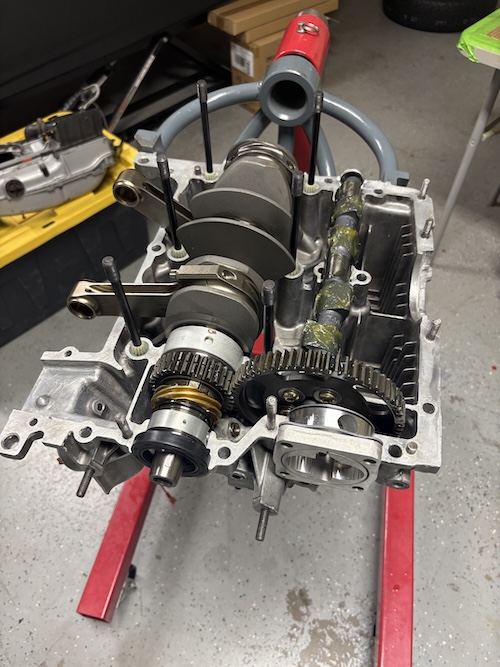
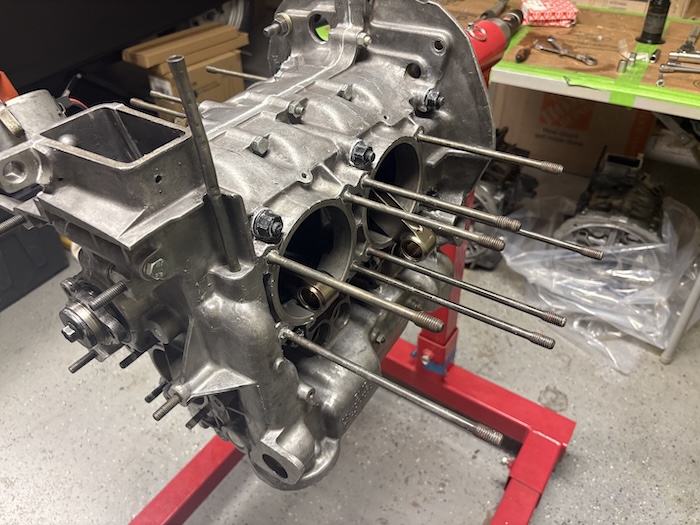
Here's the assembled short block. I did run into a problem with the oil pump. It was already clearanced for the cam bolts but the snout of the pump was actually bottoming out where the drive gear locks into the center of the cam. And it only happened once the pump was torqued. And it locked the cam/crank solid too! Scared the crap out of me. Not surprised, though. I've never worked with these special straight cut sprockets before. I work to get this problem solved next. More on this soon.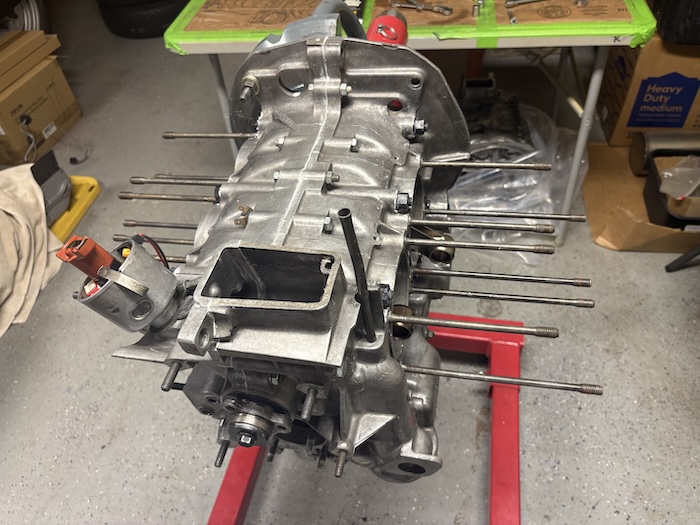
Posted by: Jack Standz Aug 24 2026, 12:52 PM
@http://www.914world.com/bbs2/index.php?showuser=4366 Standz, note I’m using a 9inch wheel here. Anything larger would probably get in the way of easily replacing the offset washers on the cam. I’m good with splitting the case again for the oil pump install but with a normal pump you could just install it and move on.
Hi Fred, thanks for the info and photo. Not sure how large the diameter our degree wheel is, but will check. Think it's a Moroso.
Also, we have a straight cut set of cam gears too for the 2615 project. Because we think the thrust bearings would take a beating using helical cam gears (even though we modified a set). Still wish a larger LSA cam was available, at least as an option. But, since they aren't available, one less decision to make
We appreciate you for documenting your build and sharing . Thanks!
Posted by: friethmiller Aug 24 2026, 01:39 PM
...
Also, we have a straight cut set of cam gears too for the 2615 project. Because we think the thrust bearings would take a beating using helical cam gears (even though we modified a set). Still wish a larger LSA cam was available, at least as an option. But, since they aren't available, one less decision to make
We appreciate you for documenting your build and sharing . Thanks!
Sure thing! Please avoid all my missteps and mistakes
 My heads are mod'd pretty good and are running double springs so I'm going with the noisy gears. Stay tuned to how I figure out my clearance issue with the oil pump. The metal must come off from the pump and/or the bolt heads. I've got the bolts in with red loctite now so heating them to 500F to back them out might not be an option. I hope to not have to split the case either. We'll see.
Posted by: porschetub Aug 25 2026, 12:21 AM
...
Also, we have a straight cut set of cam gears too for the 2615 project. Because we think the thrust bearings would take a beating using helical cam gears (even though we modified a set). Still wish a larger LSA cam was available, at least as an option. But, since they aren't available, one less decision to make
We appreciate you for documenting your build and sharing . Thanks!
Sure thing! Please avoid all my missteps and mistakes
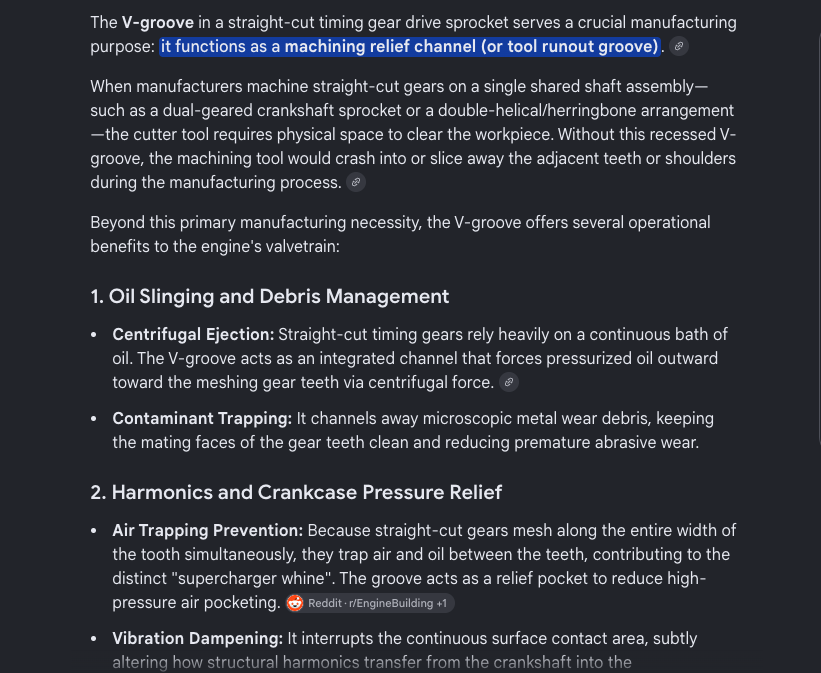
My heads are mod'd pretty good and are running double springs so I'm going with the noisy gears. Stay tuned to how I figure out my clearance issue with the oil pump. The metal must come off from the pump and/or the bolt heads. I've got the bolts in with red loctite now so heating them to 500F to back them out might not be an option. I hope to not have to split the case either. We'll see.Great progress, question is the relief cut (vee ) in the driven gear to reduce oil foaming or some reduction in noise ? , don't know much about these conversions but the T1 guys mentioned increased noise ? thanks and good luck .
Posted by: friethmiller Aug 25 2026, 09:17 AM
... question is the relief cut (vee ) in the driven gear to reduce oil foaming or some reduction in noise ? , don't know much about these conversions but the T1 guys mentioned increased noise ? thanks and good luck .
Had to search it. It does a lot of things to include the items you mentioned.
Attached image(s)
Posted by: friethmiller Aug 25 2026, 03:50 PM
Oil Pump Clearancing (8/24/2026):
Well to get the clearance necessary I had to remove the cam bolts one at a time using heat to loosen everything up. Didn't have any troubles but I did take it easy. I certainly didn't want to strip out the allen heads.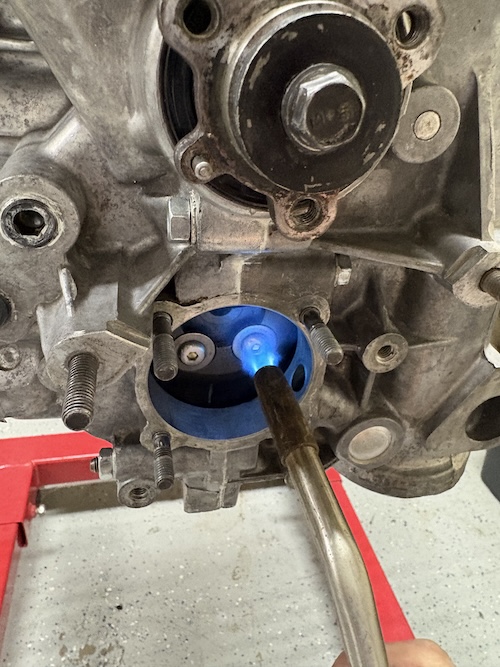
Each bolt was then mounted securely in the vise and filed down/sanded by hand/cleaned. Next, the washers were sanded to smooth out any imperfections. I had to eliminate anything that might prevent the washers from sitting flush in the gear. The next pic shows a bit of work to the pumps drive gear. I used a black marker to help identify any contact/rub points. I also sanded any rough edges on the gear teeth. 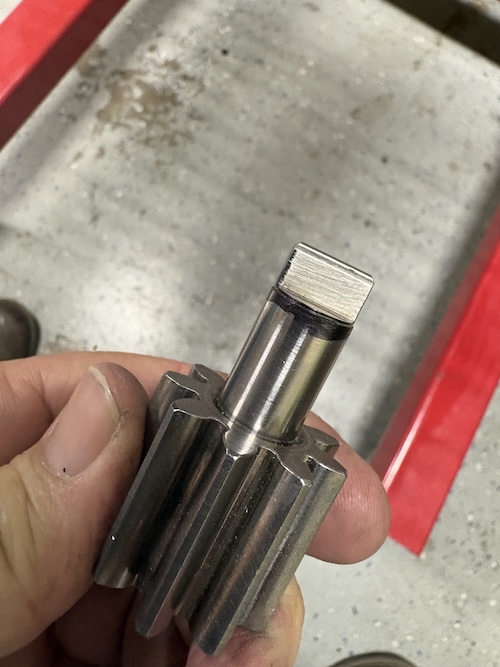
Next two photos show the relief to the back of the pump and the cam bolts. I think ideally the cam gear bolts might need to be counter-sunk into the cam washers. Not sure if this is even possible, though. 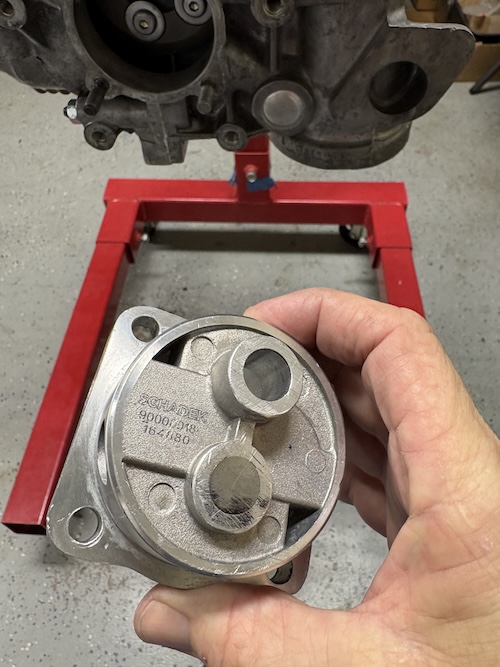
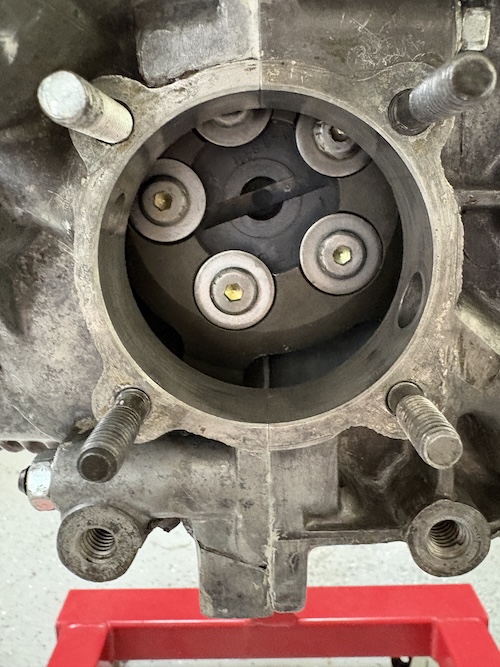
So, after test fitting everything without a gasket and getting everything to clear properly with the pump bolts torqued down, I was finally ready for reassembly. After having to insert/remove this pump about 30 times, I had developed a technique for getting the pump perfectly lined-up to go in with one push. So, I decided to roll the dice and insert the pump with the o-ring. You can see in this pic that I've prep'd the gasket (both sides with Curil-T) and used a little bit of assembly lube on the pump body and gasket. I also applied a little bit of lube to the oil pump bore on the case to help protect the o-ring as it went in. And....... after a few tense moments of making sure of my alignment, I was able to push the pump in place. I'm 99.9% sure that the o-ring is still good and right were it needs to be. 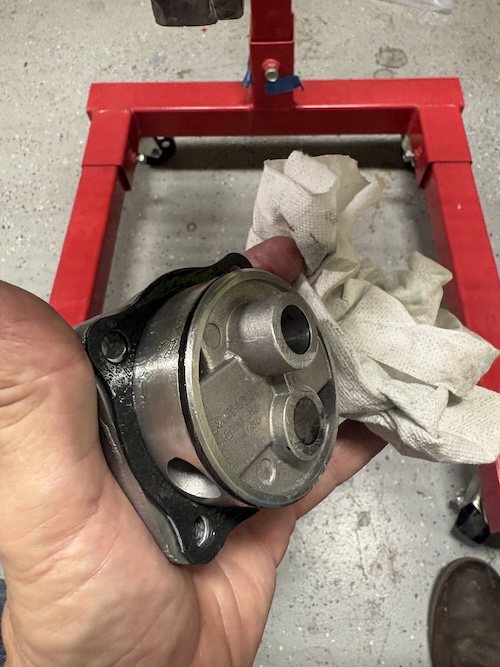
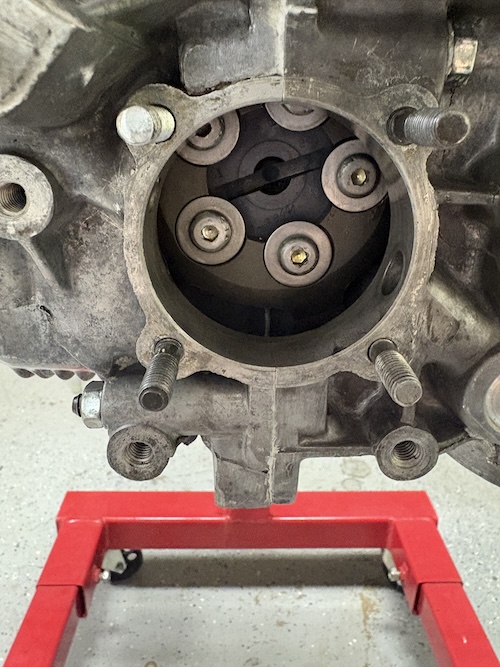
I also took a pic of the thickness of the pump gasket. It's over .060". I wasn't sure what it might crushed down to after torquing but I was glad to have a little more clearance b/w the pump & gear.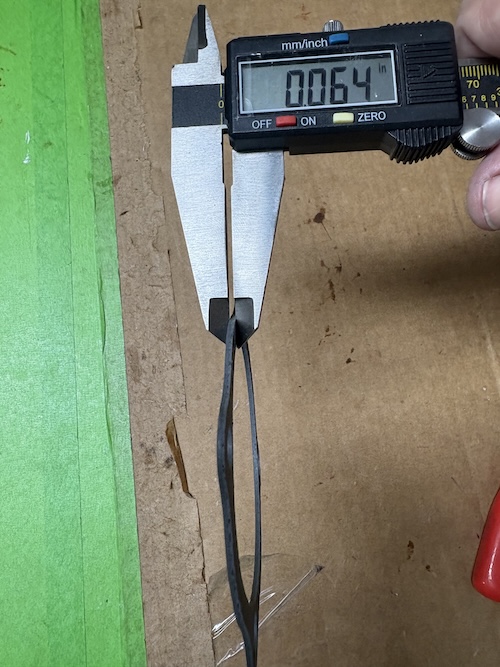
Once the pump was in, I focused on cleaning and preparing the cover. This cover was used before and you can see I had a little interface issue with the previous pump. However, I think I have this pump is a little better prep'd. Again, a very light coat of Curil-T on both sides of the paper gasket. Cover went on, and then finally the nuts/washers with a bunch of thread sealant.
I then tested that the engine rotation was good about 3 times during the torque sequence. The final test was good to go. I had full unbinding engine rotation using one hand on the crank's snout bolt. 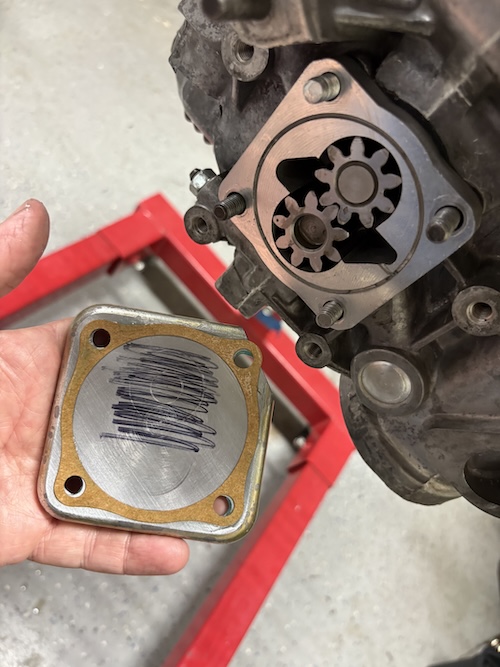
Onward! Cheers!
Posted by: friethmiller Aug 26 2026, 03:55 PM
Crankshaft End-play (8/25/2026):
I had 7 shims to work with last night. I had to take up most of the .050" that I initially measured without shims - targeting the magical .003 - .005 range. After a few tries I was finally able to get 0.003. It's a consistent .003 - .0035 too. 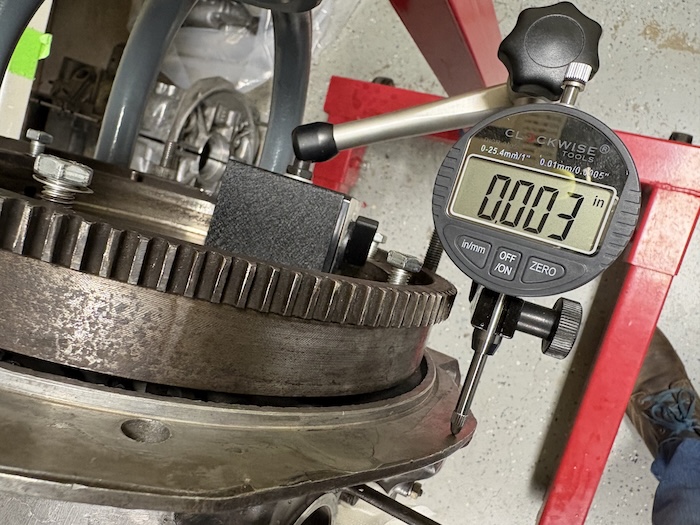
Moving on... Pistons and Cylinders are next!!
Posted by: friethmiller Aug 27 2026, 12:53 PM
Preparing Pistons & Cylinders (8/27/2026):
In preparing for pistons and cylinders this weekend, I cleaned up the work tables and pulled out all the parts and tools I'll need for this next phase of the build. I also took the opportunity to add the small items to the engine to help get stuff out of the way.
Installed the high and low pressure reliefs, front engine mounts, oil filler tower as well as the oil plug, oil screen, and inspection/taco plate.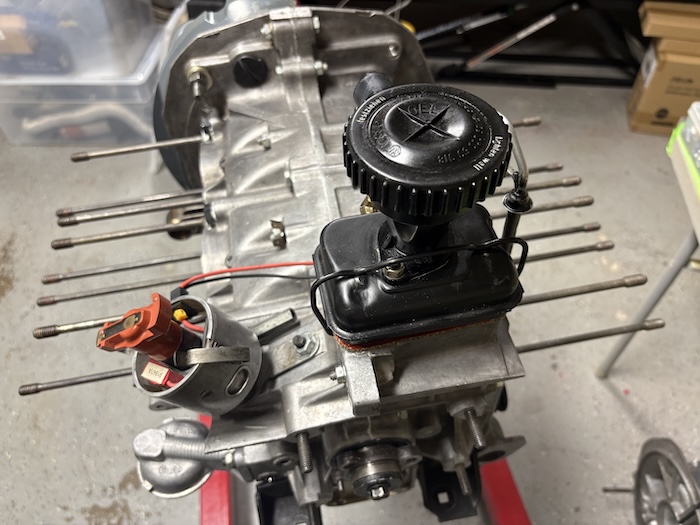
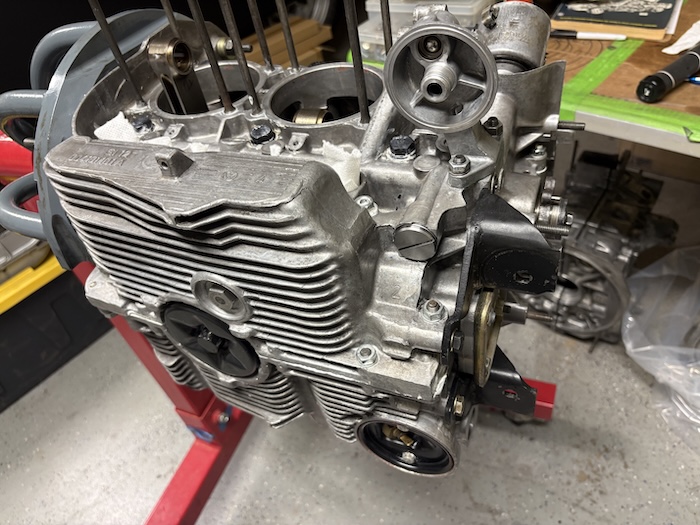
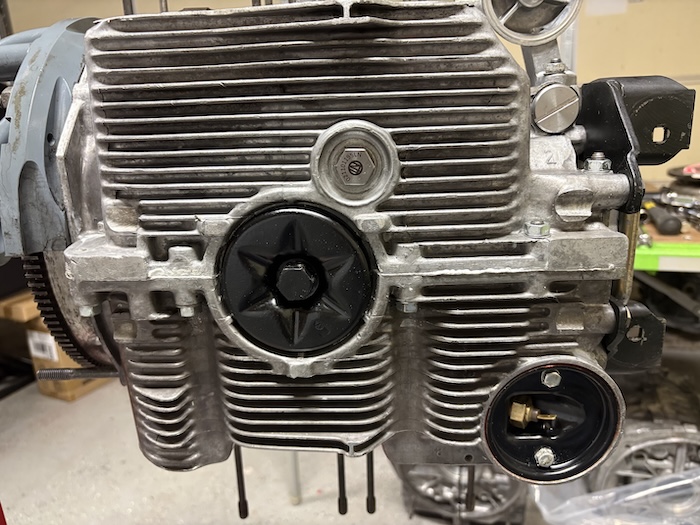
Ring End Gap
I've got 96mm cylinders; so that's 3.78". Based on the supplied chart, this would calculate as 3.78" X 0.0045" = 0.017". Can this be right? The difference between the JE and the KB piston gap is pretty substantial, I guess.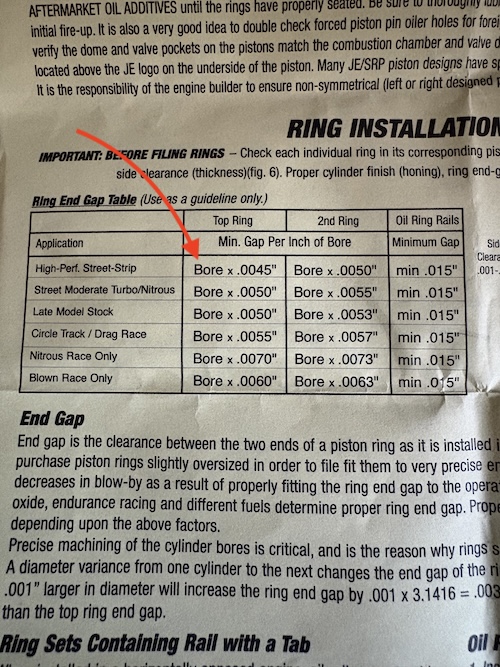
Cylinder Wall Gap
I'm also looking at Piston to Cylinder Wall Gap. I got a new battery in the 3-4" micrometer, zero'd it, and then took this initial measurement on one of the pistons. Spec says measure point is 0.5" up from the bottom. More to come on this soon.
Weekend goal is to, at a minimum, have the P&Cs 100% ready to install. The cylinder shims that I ordered from AA should arrive tomorrow so I'm hoping to everything in and ready for heads/value train by late Sunday. We'll see. Cheers! 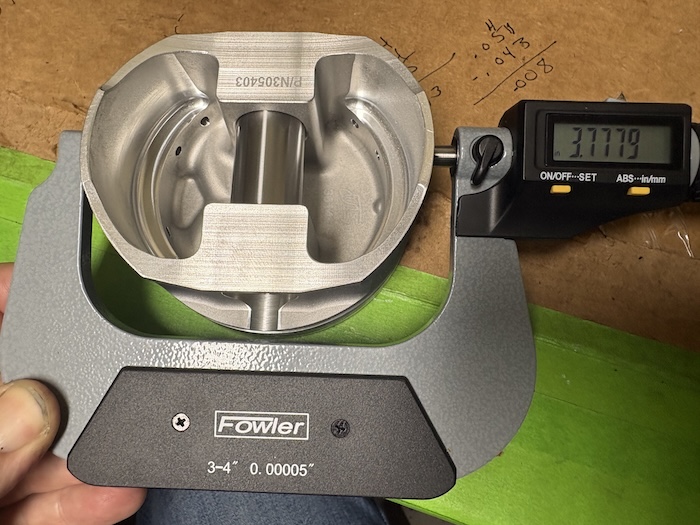
Posted by: friethmiller Aug 27 2026, 03:35 PM
@http://www.914world.com/bbs2/index.php?showuser=29004 et. al.
What about this? AI says looser is safer for air cooled.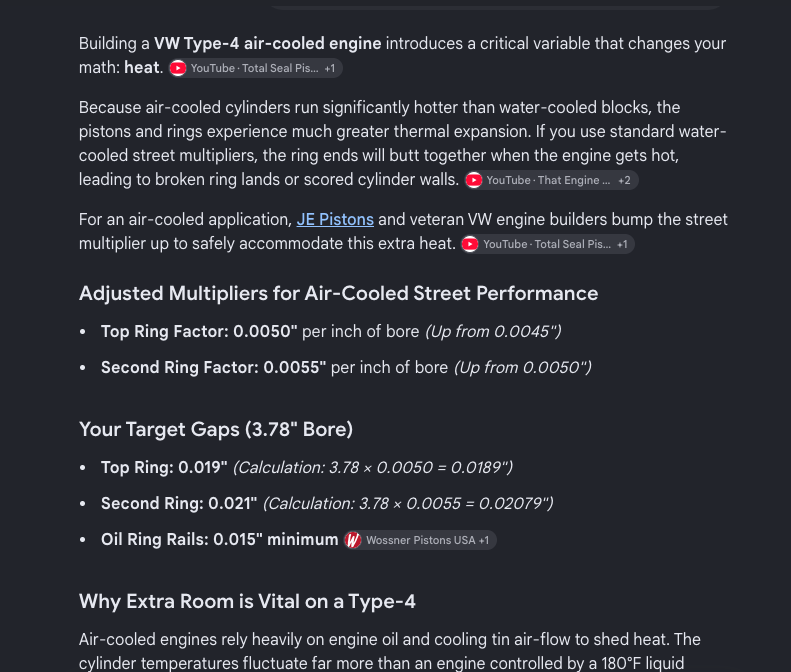
Posted by: Ninja Aug 27 2026, 05:52 PM
If you're too tight the Grim Reaper will appear and you will be the recipient of further Type 4 education.
If you're too loose, you will have slightly more blow by and MAY see higher oil consumption.
In this case I would go loose...
Forged pistons would add a little clearance as well in my book.
High RPM race type use would add more...
Posted by: friethmiller Aug 27 2026, 08:42 PM
If you're too tight the Grim Reaper will appear and you will be the recipient of further Type 4 education.
If you're too loose, you will have slightly more blow by and MAY see higher oil consumption.
In this case I would go loose...
Forged pistons would add a little clearance as well in my book.
High RPM race type use would add more...
Thanks Rick!
I've received enough "Type 4 beat-downs" for two lifetimes. I'll go with the recommended looser gaps, thank you very much.

Posted by: porschetub Aug 28 2026, 12:16 AM
If you're too tight the Grim Reaper will appear and you will be the recipient of further Type 4 education.
If you're too loose, you will have slightly more blow by and MAY see higher oil consumption.
In this case I would go loose...
Forged pistons would add a little clearance as well in my book.
High RPM race type use would add more...
Thanks Rick!
I've received enough "Type 4 beat-downs" for two lifetimes. I'll go with the recommended looser gaps, thank you very much.
Great response
 perhaps my reply would have been less polite,end of the day you know what you are doing besides .
Cheers and keep up the good work .
Posted by: Jack Standz Aug 28 2026, 12:39 AM
Maybe take a look at this post:
https://shoptalkforums.com/viewtopic.php?t=1505
However, Raby has said some conflicting things about ring gap over the years (possibly due to his experience with specific ring manufacturers like Deves or Hastings) and that he generally doesn't like too large a ring gap. Lately it seems he doesn't publish his ring gap recommendations, probably to avoid arguments. But, he's built a lot of type iv motors and backs up what he says with test results.
Would really like to get some GT3RS rings that he has recommended to run in our JE pistons with nickies cylinders (102mm), but they don't fit our custom pistons!
Posted by: friethmiller Aug 28 2026, 03:39 AM
Maybe take a look at this post:
https://shoptalkforums.com/viewtopic.php?t=1505
However, Raby has said some conflicting things about ring gap over the years (possibly due to his experience with specific ring manufacturers like Deves or Hastings) and that he generally doesn't like too large a ring gap. Lately it seems he doesn't publish his ring gap recommendations, probably to avoid arguments. But, he's built a lot of type iv motors and backs up what he says with test results.
Would really like to get some GT3RS rings that he has recommended to run in our JE pistons with nickies cylinders (102mm), but they don't fit our custom pistons!
Yeah, this is an older thread but it sounds like he was saying .019, which aligns with AI’s recommendation here. Interesting. I’m moving forward though. Having a set of Nickies would be awesome. Can’t imagine what your big 2.6 motor is going to sound like.

Posted by: HFC3 Aug 28 2026, 06:18 AM
I don't feel worthy of even reading your posts, but my appreciation and admiration for you and your fellow engine builders is high! Great job.
Posted by: friethmiller Aug 30 2026, 04:01 PM
Piston to Cylinder Wall Clearance (8/29/2026):
Thought I'd verify the clearance for the pistons before moving any further along with the build. The spec for these 2618 forged pistons calls for a large .0035 to .0040" gap. Surely the 93mm pistons that I had the machine shop bore to 96mm would have pull my pistons off the engine cart and verify proper clearance. NOPE! 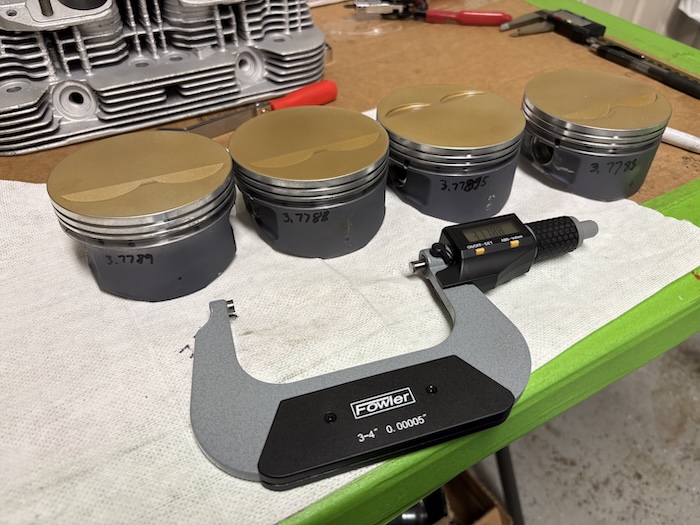
After mic'ing all the pistons and taking an I.D. measurement of each of the cylinders (several spots up/down at two different clock directions) the numbers I was getting were between 0.0005" and 0.0000" of clearance! I verified this by taking one of the pistons without rings, turned it upside down and watched it stick in the bore. NOPE! I then sent a text to the machinist, his reply was that he thought he had seen his assistant taking these measurements. This was not the right answer. He said I could send them back and have them check and recut the cylinders. I thought about this for a minute or two and then realized how extremely slow this shop was at doing anything. Nope!
Then it hit me. I've got a perfectly good set of KB stoker pistons sitting on the shelve. So, I pulled them out, cleaned them up, and started taking measurements. These pistons measured smaller than the JE pistons and produced excellent numbers on all my clearance checks. Plus, the KB are hypereutectic and allow for tighter clearances. Below pics show my piston measurements and one of many clearance checks made on each cylinder.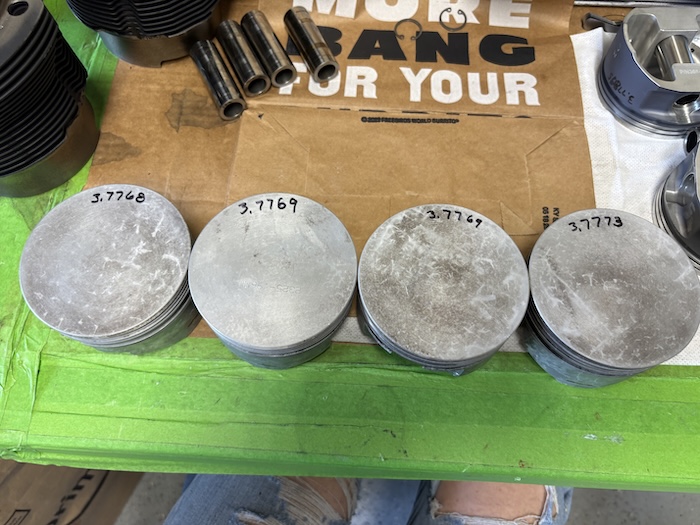
Here's a chart I made of the measurements. These are right in-range for these KB pistons.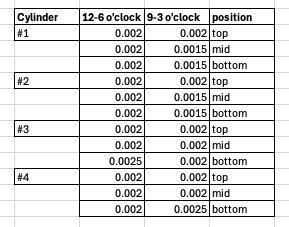
So, my decision was to go with the KBs and use the JEs on a different build I plan to do next year. First pic shows a little clean up on any sharp edges before cleaning the pistons again in the ultra-sonic cleaner. Second and third photos show me taking an initial deck height on piston #1. Roughly figured I needed a .060 or .050 shim to get in the .045 - .050 deck height range. Depending on the final number, the engine compression will be between 9:1 to 9:2. So, the only thing holding me up from moving forward is a new set of KB piston rings. More to come soon on this... standby. 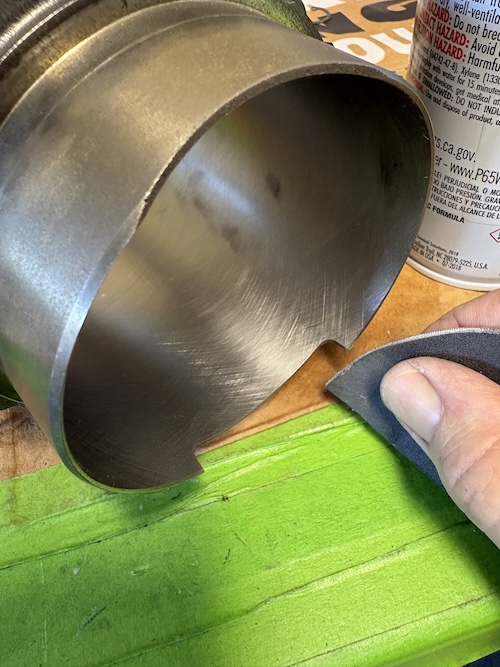
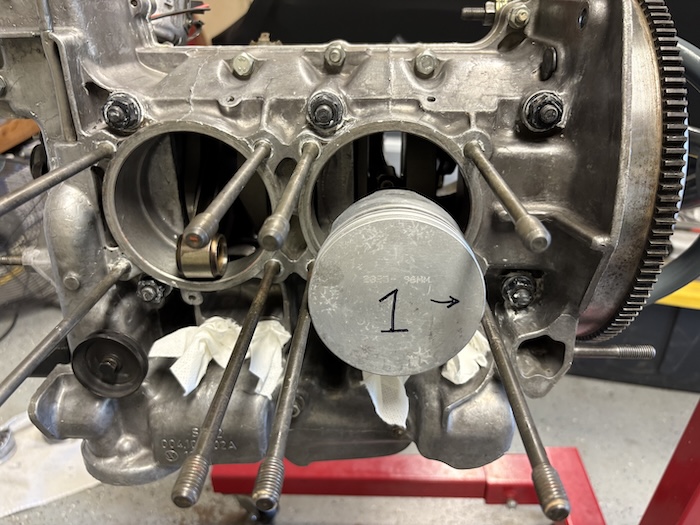
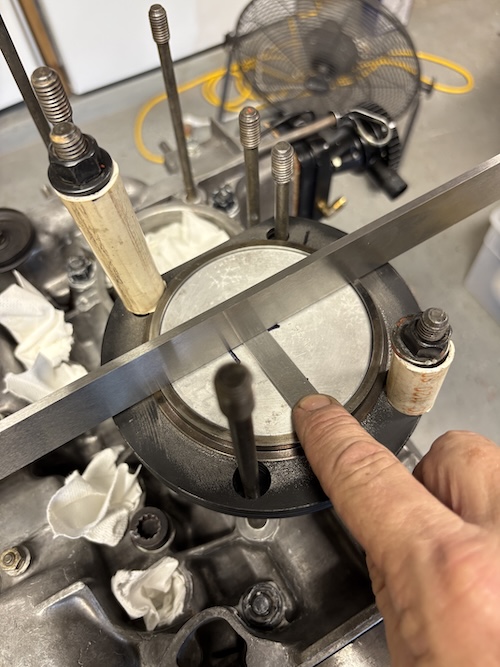
Posted by: friethmiller Aug 30 2026, 04:18 PM
Saturday Evening Bonus - Flywheel, Clutch, and Pressure Plate Assembly (8/29/2026):
Working down the to-do list here. With the crank's end-play figured out, I was ready to pull out the shims, cleaned them up, clean the back end of the crank/case area, and prepare everything for final assembly. With the shims back in place, I then installed the rear main seal and added some oil to prevent any burn-up durning startup (pic 1). The second photo is my silly attempt at switching to a new flywheel but this was quickly ruled out. 1) It wasn't balanced with the rest of the assembly; and 2) I checked the end-play and it was too tight (like .0005). So, I smartly reverted back to my original flywheel and verified a .0035 float [again]. I'll leave that new flywheel for another build. 
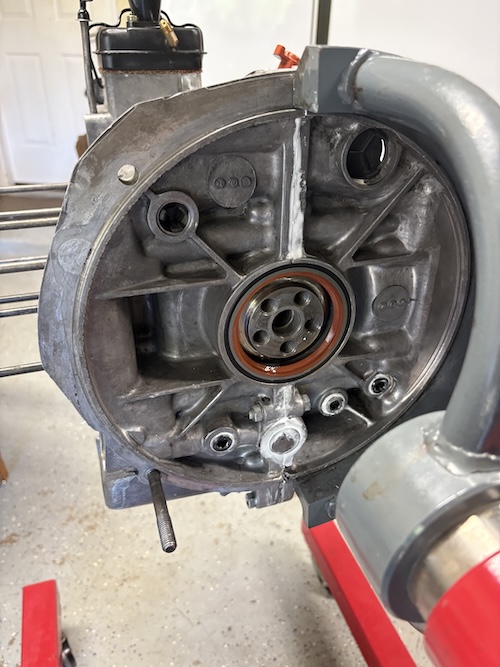
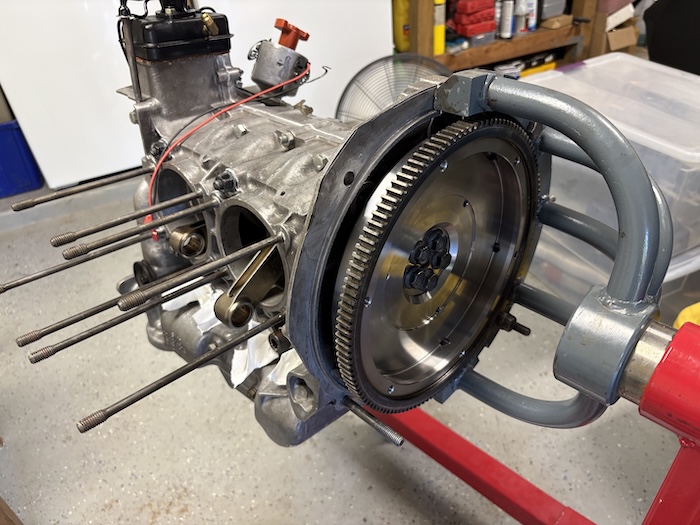
Final photo here shows the flywheel, clutch, and pressure plate all cleaned up and installed. Done! 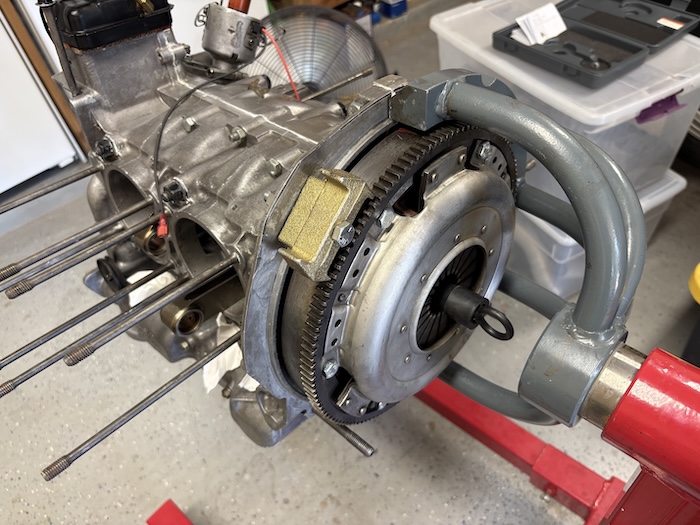
Posted by: friethmiller Aug 30 2026, 04:33 PM
Initial Oil Cooler Work - Part 1 (8/30/2026):
Quick post on my initial work on installing the Tangerine Racking remote oil cooler kit. I thought I'd start my Sunday morning re-reading the instructions. After a second cup was finished, I was finally ready to do this part of the install.
The first pic shows the two custom studs that were inserted with thread-locker. These work with the original 3rd stud to secure this mounting plate. Note the orange seals and the use of a (provided) spacer for the original stud.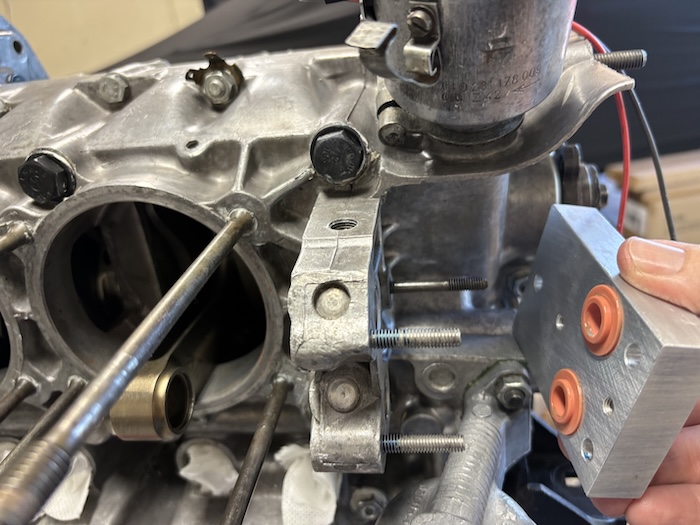
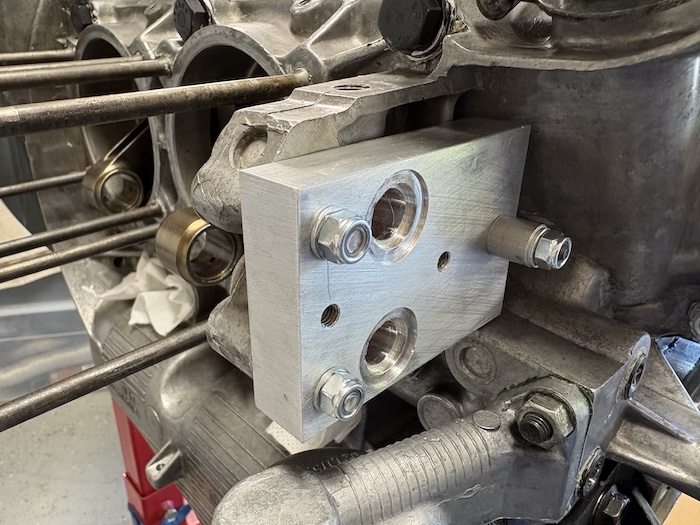
This plate is what holds on the next part. This aluminum block houses an internal thermostat. This mounts to the plate with two long bolts and another set of recessed orange seals. Final photo shows the assembly completed with the large 10AN inlet/outlet. The other parts of this kit will be installed later.
Posted by: friethmiller Aug 30 2026, 04:44 PM
Prep'n Valve Train and Verifying Deck Height (8/30/2026):
While I wait for new piston rings, thought I'd take some time to clean-up the garage a bit and reorganize things for the coming valve-train work.
I had that Tobari guy do 2 sets of rockers for me several months ago so I figured it might be a good time to pull everything out and get everything ready for install. One set of rockers are 10mm and go to this engine, the other set are 8mm that I pulled off an old 1.7L engine of mine. This smaller set or rockers will like be used for the LE's 2.0L, which will be rebuilt right after this engine is finished. First pic shows the parts getting ready for a round in the hyper-sonic cleaner. The second photo is everything ready [with other parts] for the upper assembly install.
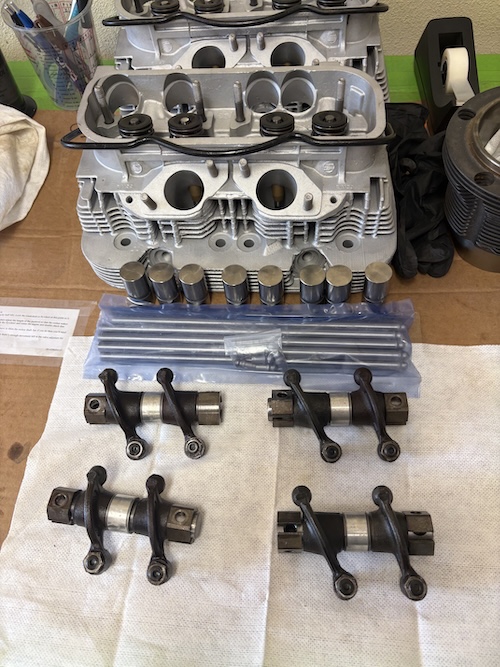
Verifying Deck Height
With the extra time I had, I thought it might be worth my while to verify deck height on all my cylinders. Glad I did. Looks like going with the .050" shim. I did note a slightly different deck height b/w the two sides of the engine. The 1 & 2 cylinder side measures at .046 and the 3 & 4 cylinder side is at .048. Not sure if that going to cause any problem. Here are few pics of my engine during this process. The cylinders look good. Everything checks out flat! That's all for today. Hopefully more soon once the rings arrive. Cheers! 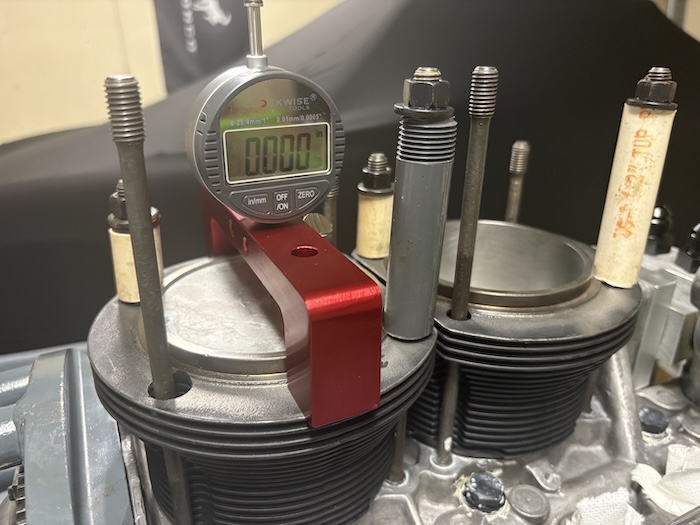
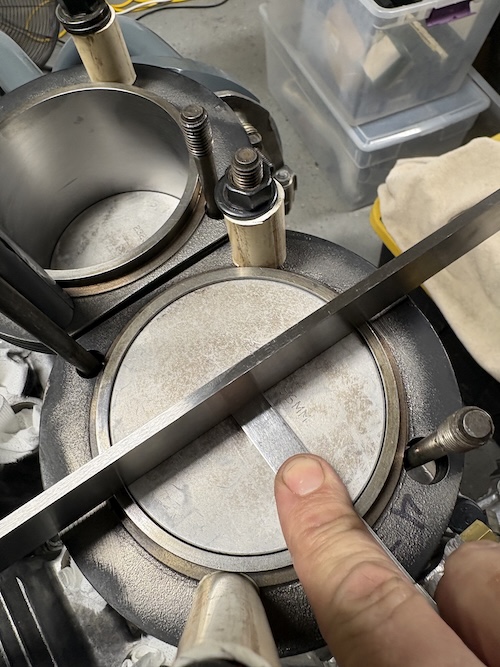
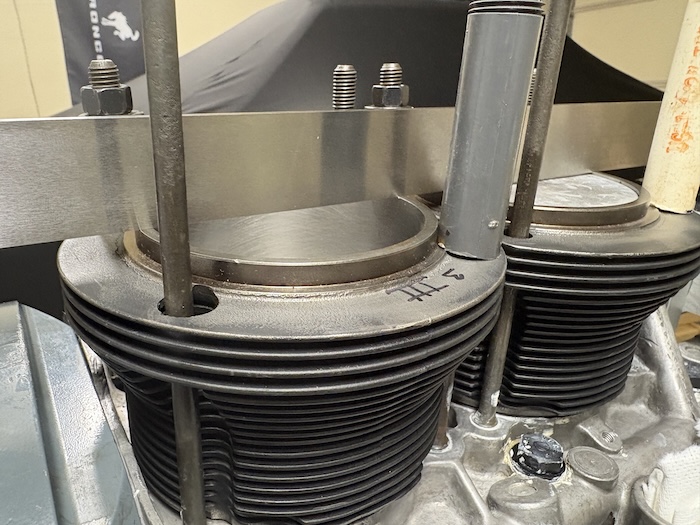
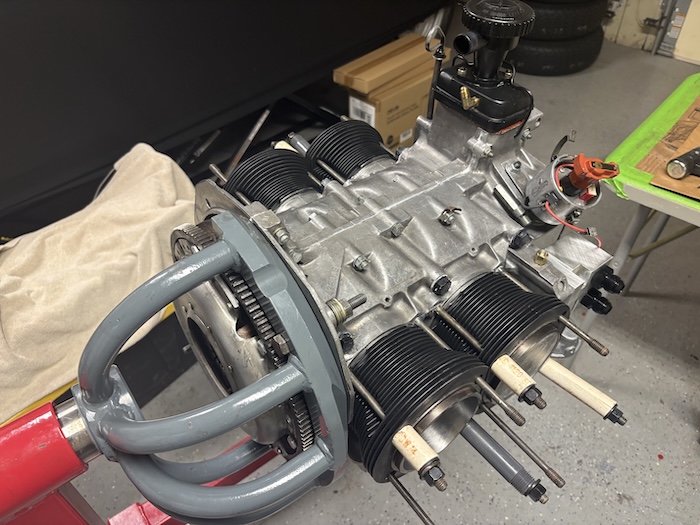
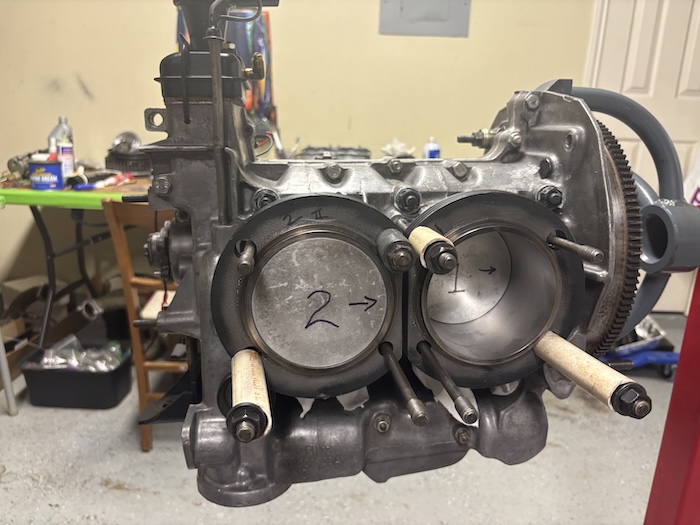
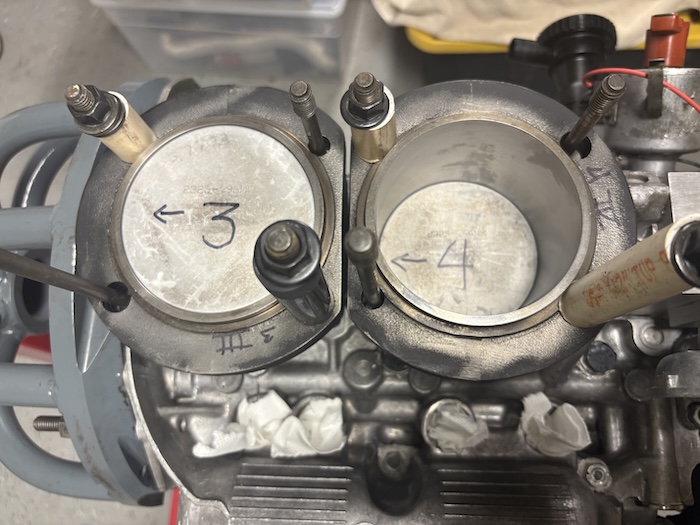
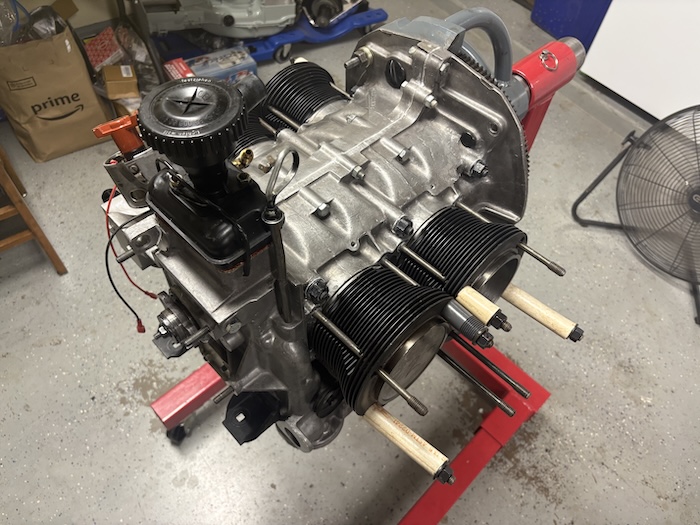
Posted by: Ninja Aug 30 2026, 05:01 PM
You SHOULD tighten up deck height numbers when using the hyper-eutectic KBs.
I'd be hunting .038 to .044.
Will increase compression a tiny bit.
Will increase quench action substantially.
Both effects increase power with zero downsides as long as you don't kiss a head.
Running quench this tight means verifying all 4 cylinders!
Your .002+ numbers look great for the KBs.
I'd ceramic coat those flat tops.
I prefer a true flat-top piston over everything else as long as you can achieve a decent compression ratio and clear the valves.
With your cam I'd CAREFULLY check piston to valve clearance as you will be getting close with those.
Did the JEs have valve cuts in the crowns?
Posted by: friethmiller Aug 30 2026, 05:20 PM
Did the JEs have valve cuts in the crowns?
Yes. They added 0.9 cc to the combustion chamber, too.
With the flat top KBs and a 0.045 - 0.047 deck height, that will put me at 9.2 CR. Getting shims to dial things in seems to be a problem, Rick. If you can @#$! out these off sizes please put them in the mail to me, ASAP
Posted by: Ninja Aug 30 2026, 08:27 PM
Nope, don't have any shims at all.
I can do the math just fine.
You posted your last post while I was making mine, and I didn't see that you had ALREADY checked all 4 (I wouldn't have said anything).
What you came up with will work fine.
I'd prefer to be a little tighter but it's probably not worth the headache.
The SEVERE lack of good/correct/adjustable Type 4 parts is one of the main reasons I won't be walking this path.
The lack of decent machine shops is another. The one you used is the one I'd count on and it doesn't look workable anymore.
For sure you need to check Piston/valve clearance as that was the limiting factor with a true flat top. Those eyebrows the JEs have are BIGTIME useful. They also make the crown thicker and the overall piston heavier. Those KBs are lightweight pistons.
About two years ago I did research shims, pickings were slim then but looked still doable.
What is possible if you have too much clearance is to have the tops of the jugs flycut the exact correct amount. Once again, you are at the mercy of the machine shop.
This is how I set piston-head clearance on everything else; Deck cut.
On normal water cooled (without multiple head gasket thickness available) going too far means another block or fly cutting pistons.
Forged/cast can be fly cut but hyper cannot without diamond tipped cutters.
If you've got any type of dome/rise in the crown you're screwed on fly cutting pistons.
Fly cutting pistons weakens them too.
The trick is getting the deck cut right.
You are doing it RIGHT! You are making the right choices and trying to buy the right parts. I'm not seeing any corner cutting. You are kicking ass!
The really sad thing is that after doing this whole dance spending all this money you will be lucky if you hit 180HP and it lasts 50k.
You should already know but in case you forgot little baby ROLL PINS in the lower oil control ring groove are a requirement on the KBs.
Posted by: friethmiller Aug 30 2026, 09:25 PM
You should already know but in case you forgot little baby ROLL PINS in the lower oil control ring groove are a requirement on the KBs.
Yes, you know I know this
. The new rings should be correct but I will verify when they show up. I think these come with a full 360 degree bottom oil ring with a detent that prevents rotation. We'll see.
Posted by: Jack Standz Aug 31 2026, 11:06 AM
You are doing it RIGHT! You are making the right choices and trying to buy the right parts. I'm not seeing any corner cutting. You are kicking ass!
The really sad thing is that after doing this whole dance spending all this money you will be lucky if you hit 180HP and it lasts 50k.
Although, there was a time when getting 180 HPs from a type iv was a dream. The original 914/6 put out a "whopping" 110 HPs. Our 2 liter 4 cylinder motor meets/exceeds that.No doubt that you will enjoy 150+ aircooled HPs in this 914.
As for being 2 thousandths difference between the decks, that's not an issue. A much bigger issue is air getting into the motor in a synchronized/balanced manner (which is why we're considering developing a plenum with a single throttle body/aftermarket FI) even though we already have a new dual throttle body intake system. But, if you've already settled where you're heading with the intake system, you'll be fine.
Very much enjoy watching your project(s) and your careful design and build. Go Fred!!
BTW The Type IV Store has some blanchard ground spacers in stock for certain thicknesses. They should (used to) sell custom sizes? Not sure what the lead time might be if they still offer them.
Posted by: Ninja Aug 31 2026, 11:31 AM
I remember finding a source for custom ground stuff. Long lead time, a little expensive but it looked like they were "retiring" or ending the business.
This was 2 years back. I did buy a set of extended length head studs as I figured I might need them...
LN looks like one of the few good sources left.
Just a bit pricey for my taste.
The T4 cost per horsepower is higher than almost anything else nowadays.
911 horsepower/dollar is not a good ratio either...
Posted by: friethmiller Aug 31 2026, 01:17 PM
Good input guys. Thanks.
If I run .040" shims + either a .010" or a .08" shim (that I found this morning in my a box of engine components), I can now get a deck height of .046 on both sides of the engine. That puts me at a CR of 9.2. One shim is best, I know, but I'd rather have equal deck height running two shims.
I'm set to clay the piston/valve clearance this evening, if I can cut down my adjustable push-rod. The clay is already in the #1 cylinder and torqued down ready to go.
It's basically round the clock engine building whenever I'm not working to pay the bills.
Posted by: Ninja Aug 31 2026, 01:25 PM
Make sure the shim packs are exactly the same on adjoining cylinders.
You can have different sizes across the engine but must be the same for both cylinders on one bank.
You can have trouble sealing jug to head is they are different on one bank.
Posted by: friethmiller Aug 31 2026, 01:29 PM
Make sure the shim packs are exactly the same on adjoining cylinders.
You can have different sizes across the engine but must be the same for both cylinders on one bank.
You can have trouble sealing jug to head is they are different on one bank.
Yes, I've got a total of .050" on the 1&2 bank, and .048" on the other.
Posted by: 930cabman Aug 31 2026, 01:31 PM
Make sure the shim packs are exactly the same on adjoining cylinders.
You can have different sizes across the engine but must be the same for both cylinders on one bank.
You can have trouble sealing jug to head is they are different on one bank.
A recent 2056 build I used small strips of Plasti Gage at quarter points at the top of the cylinders when I did a trial cylinder head fit to compare how true the sealing surface ( cylinder to head) connection was. It gave me good information, bolted everything up without a gasket and 20k miles later she is still running great.
Posted by: friethmiller Aug 31 2026, 05:16 PM
Make sure the shim packs are exactly the same on adjoining cylinders.
You can have different sizes across the engine but must be the same for both cylinders on one bank.
You can have trouble sealing jug to head is they are different on one bank.
A recent 2056 build I used small strips of Plasti Gage at quarter points at the top of the cylinders when I did a trial cylinder head fit to compare how true the sealing surface ( cylinder to head) connection was. It gave me good information, bolted everything up without a gasket and 20k miles later she is still running great.
Nice! That's a good idea
Posted by: 930cabman Aug 31 2026, 05:41 PM
Make sure the shim packs are exactly the same on adjoining cylinders.
You can have different sizes across the engine but must be the same for both cylinders on one bank.
You can have trouble sealing jug to head is they are different on one bank.
A recent 2056 build I used small strips of Plasti Gage at quarter points at the top of the cylinders when I did a trial cylinder head fit to compare how true the sealing surface ( cylinder to head) connection was. It gave me good information, bolted everything up without a gasket and 20k miles later she is still running great.
Nice! That's a good idea
Cost is near zero, doesn't take much time and provides information
Posted by: friethmiller Sep 1 2026, 05:23 PM
Piston to Valve Clearance (8/31/2026):
Intake Clearance
To do this, I figured I needed to make sure my valve was meeting the spec for the max intake of .507". So, I bolted on a head and used an adjustable pushrod and dial gauge to make the necessary adjustments to hit this number. I wasn't concerned with the valve train geometry, just trying to make sure my valve was opening the required amount. Once that was accomplished, I pulled the head back off and placed clay under the intake valve area on the #1 piston.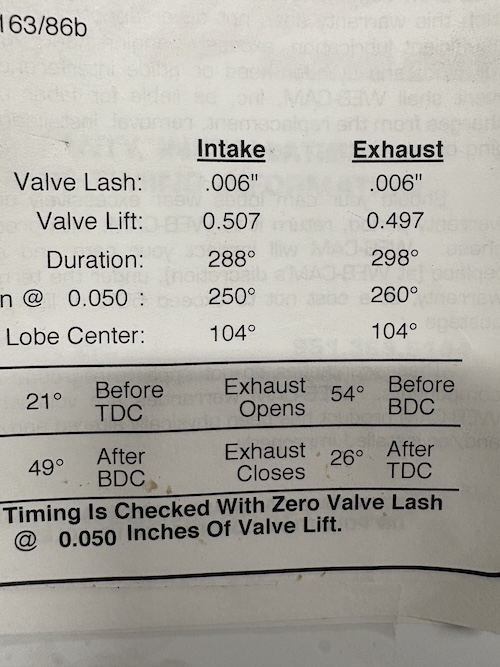
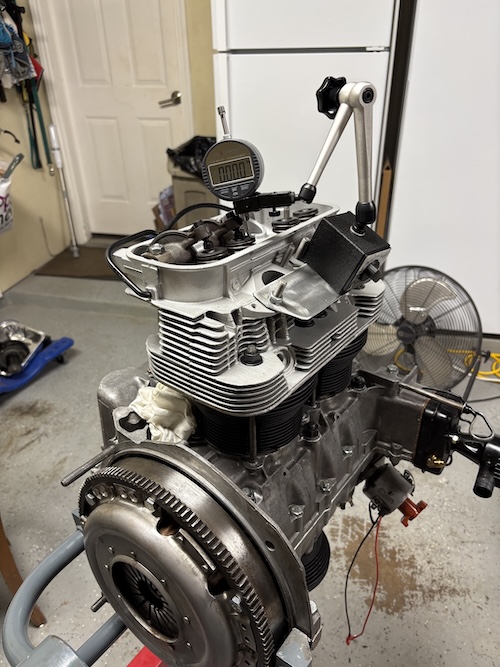
I then reattached the head, valve train, and dial gauge. After several rotations of the crank, I pulled the head, cut the clay with a razor, and exposed the profile. With my vernier caliper, I took a measurement of 0.050".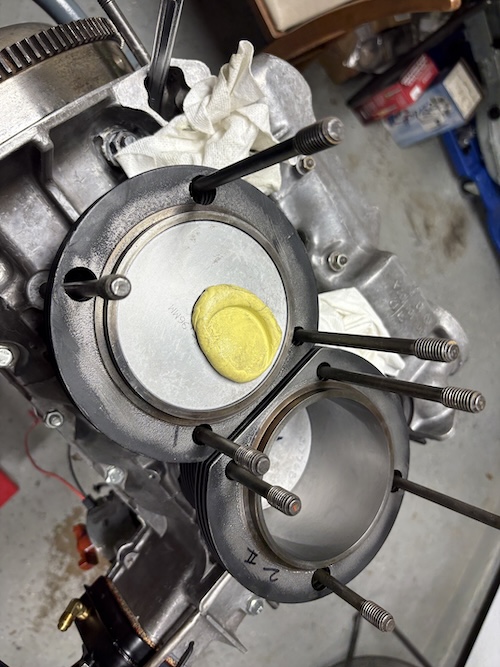
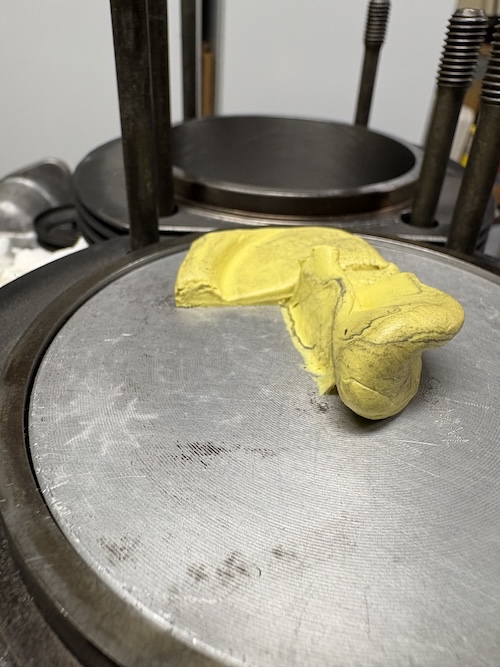
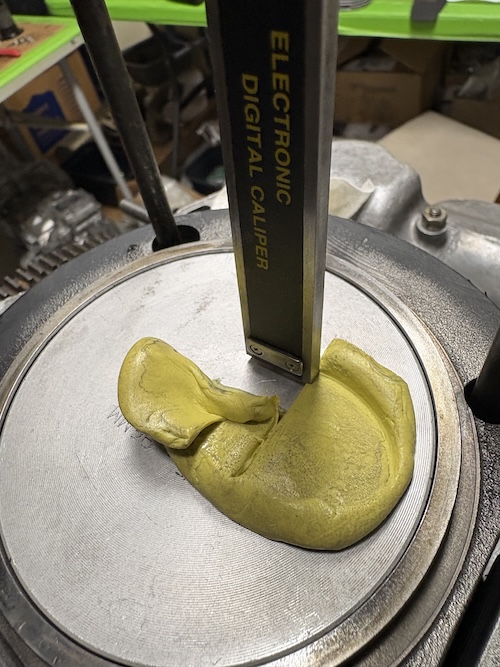
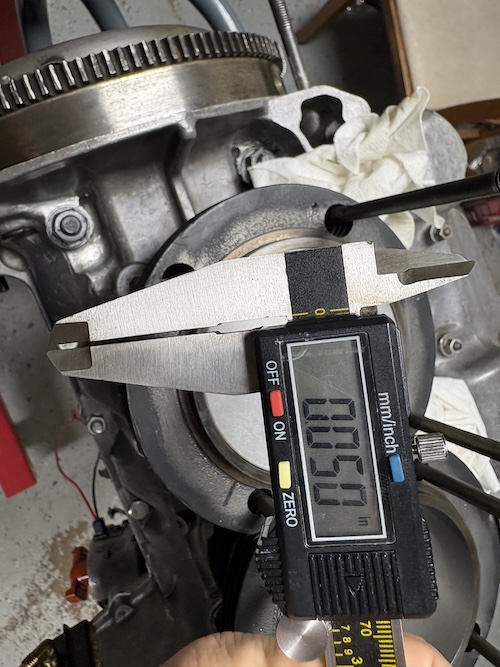
This seems too close for me!  [ @http://www.914world.com/bbs2/index.php?showuser=29004 mentioned this earlier] I'm thinking this cam and piston combo may not be ideal. I did talk with a rep at AA today. They have liners that are matched with my 2618 JE Pistons with the valve pockets. This might be the better way to go. Hmmmm.....
Posted by: Ninja Sep 1 2026, 05:49 PM
"Standard" minimum valve to piston clearance:
Intake .080
Exhaust .100
I'm not certain if Type 4 clearance recommendations are different but there's not a snowballs chance in hell that I'd run what you currently have...
Like I mentioned in my pm one of the KBs shortcomings is it cannot accommodate a serious cam.
A little tiny eyebrow would help BIGTIME on them.
There are "redneck" cutters available for use directly in the head to "cut your own" for many applications (The LS GM engines are one of them).
I have no idea if such a critter is available for VW stuff.
Doesn't really matter. Hypereutectic material is a BITCH to cut (it's the glass that screws everything up) and I would not want to use a hyper cast piston that I'd cut through the outer "skin" on the crown.
Your JEs are beautiful, use them...
Edit: on the "matched" liners...
As Ronald Regan once said "Trust but verify"!
Posted by: 930cabman Sep 1 2026, 06:52 PM
I'd play it safe
Posted by: friethmiller Sep 2 2026, 01:01 PM
I'd play it safe
Yep!
I ordered new liners that should match my JE pistons. They'll be here in a few days. In the meantime, I started moving on the GA block for the LE. I'll post my work on that engine on the other thread.
Posted by: Jack Standz Sep 2 2026, 01:32 PM
Here's what Len Hoffman says about valve to piston clearance:
Target Range for Performance Builds: 0.060"–0.080" (1.5–2.0 mm)
https://docs.lnengineering.com/article/191-measuring-piston-to-head-and-valve-clearances
Also, some say the minimum they use is 50 thousandths. We might be willing to go there or get spacers that get you up to 60 thousandths.
Good luck whatever you decide to do.
Posted by: friethmiller Sep 2 2026, 03:17 PM
...
As Ronald Regan once said "Trust but verify"!
Always!!

Posted by: friethmiller Sep 2 2026, 04:07 PM
Here's what Len Hoffman says about valve to piston clearance:
Target Range for Performance Builds: 0.060"–0.080" (1.5–2.0 mm)
https://docs.lnengineering.com/article/191-measuring-piston-to-head-and-valve-clearances
Also, some say the minimum they use is 50 thousandths. We might be willing to go there or get spacers that get you up to 60 thousandths.
Good luck whatever you decide to do.
Posted by: friethmiller Sep 7 2026, 08:44 PM
Quick Update: New cylinders showed up on Saturday morning from AA Performance. These are big bore cylinders that are meant to fit my stroker JE pistons. And, while these provide a little more room than my other cylinders, they are still too narrow. I need a minimum of .0035 of clearance. I will call AA in the morning to follow-up with other possible options. Getting these cylinders honed is probably what needs to be done.
1st pic shows the part number for these Biral liners. The second shows one of JE pistons sitting in one of the cylinders. Note: this piston is rotated about 90 degrees out of its intended position and will slide down the bore but it is no where near .0035 - .004 clearance at the 0.5" mark from the bottom of the piston skirt.
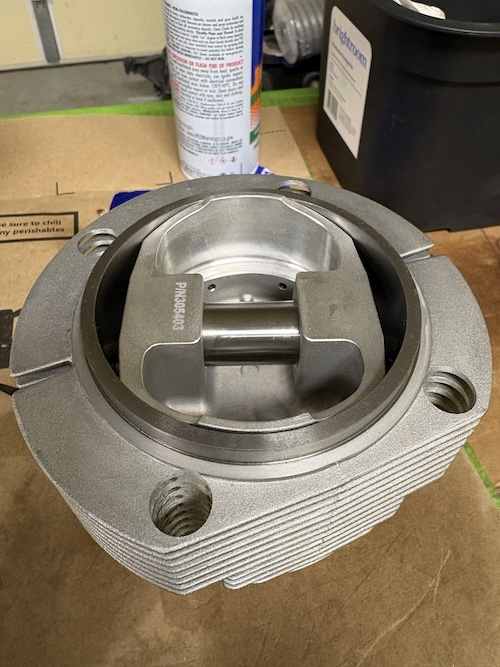
With this delay, I pulled the engine off the stand and started work on the LE's 2056 build. I will post on my other thread for that shortly.
Posted by: Ninja Sep 8 2026, 06:48 AM
There's a tag I've not seen before!
"Steel NOT made from Russia"
The one I WANT to see!
"Steel NOT made from China"
I wonder if this is the new replacement for the "Globally sourced" moniker which is on everything now.
What's holding that piston up?
Hope it's not friction! 
Those piston clearance measurements are minimums not maximums...
I once did a deep search on what the maximum clearance should be on a forged piston.
No consensus...
Some of the drag race big blocks (with power adder-NO2/blower) use as much .010!
Just flopping in the bore...
Posted by: friethmiller Sep 8 2026, 10:03 AM
What's holding that piston up?
Hope it's not friction!
Here's what I measured for each piston. The label on the box says bore of 3.779". The ceramic coating on the skirts is really light - maybe .0005". My ability to take exact measurements might be an issue here. However, getting a piston to "hang" in the bore is not a good indicator of clearance and/or ovality.
Waiting to hear back from AA on what they recommend to do.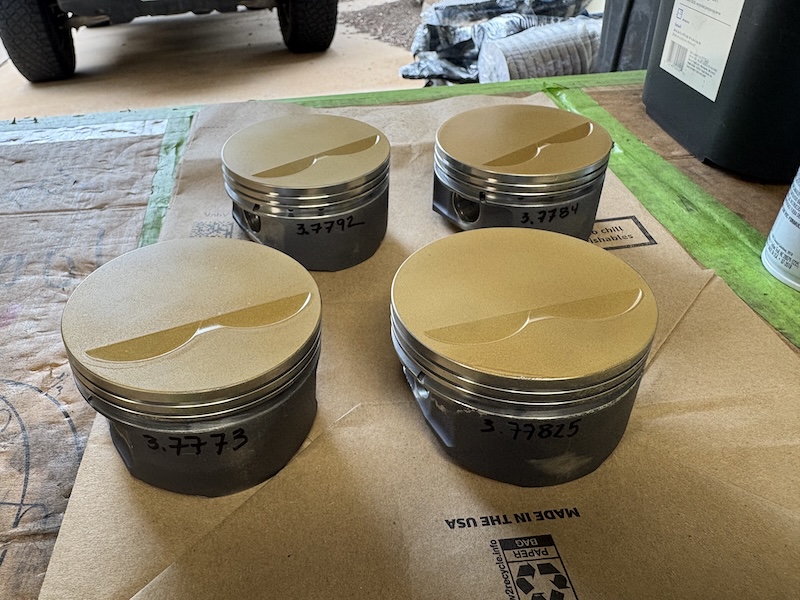
Powered by Invision Power Board (http://www.invisionboard.com)
© Invision Power Services (http://www.invisionpower.com)